TECHNOLOGY EXPLAINER
Polyimide
— infusible and insoluble, so it is built from a precursor
DuPont's Kapton HN is described as a film used in applications from −269 °C to 400 °C, and its melting point is listed as "none". The film's heat resistance and its difficulty to process have the same cause. The way around it is a two-step synthesis: shape the polymer while it still dissolves, then harden it afterwards.
- What polyimide is (the short version)
- Two-step synthesis: go through polyamic acid, then close the imide ring afterwards
- A materials engineer's view (1): "it does not dissolve," so you build it from a precursor
- The numbers: Kapton HN and UPILEX-S (manufacturers' stated values)
- Our calculation: thermal expansion and the shrinkage on first heating
- A materials engineer's view (2): what it means to have no glass transition point
- Polyimide inside flexible printed circuits (FPC)
- Polyimide in semiconductors and lithium-ion batteries
- Transparent polyimide: why it is coloured, and the road to foldable displays
- A materials engineer's view (3): what do you lose by making it transparent?
- Challenges and limits / Glossary / References / Claim-to-source audit
Sourced = a statement found in published material (link given)
Our calculation = a figure this article derived from stated assumptions
Not yet confirmed = a plan or target with no confirmed track record
Structural readings and materials-design interpretations are marked separately as commentary.
Property values are given together with the test method, conditions and source, and a manufacturer's stated value is always identified as such.
This is not an article that ranks products.
1. What polyimide is (the short version)
"Polyimide" is the name for a polymer that carries imide rings (five-membered rings in which a nitrogen sits between two carbonyl groups) in its main chain. This article deals mainly with aromatic polyimides, in which benzene rings and imide rings alternate along the chain.
- High heat resistance: Qnity (formerly DuPont) describes Kapton HN as a general-purpose film that has been used in applications at temperatures as low as −269 °C and as high as 400 °CSourced. The DuPont datasheet lists the melting point as "None" (ASTM E794)Sourced
- It does not melt, so it is made from a precursor: a DuPont patent published in 1965 describes a two-stage method. First make polyamic acid, a soluble precursor, from a diamine and a dianhydride; then, once it has been shaped, convert it to polyimide by heat or chemical treatmentSourced
- Colour, and the challenge of transparency: a paper attributes the yellow-to-amber colour of aromatic polyimide films to charge-transfer (CT) interactions. Making the polymer colourless while keeping heat resistance and low thermal expansion is described as difficultSourced
Polyimide is not "high-performance but hard to process." It is a material in which the difficulty of processing and the high performance have the same cause. The molecules are rigid and the chains attract one another strongly, so the polymer neither melts nor dissolves, and it does not soften even at high temperature. That is why it is made by fixing the shape while the material is still dissolved (the precursor stage) and setting its properties afterwards (our commentary).
2. Two-step synthesis: go through polyamic acid, then close the imide ring afterwards
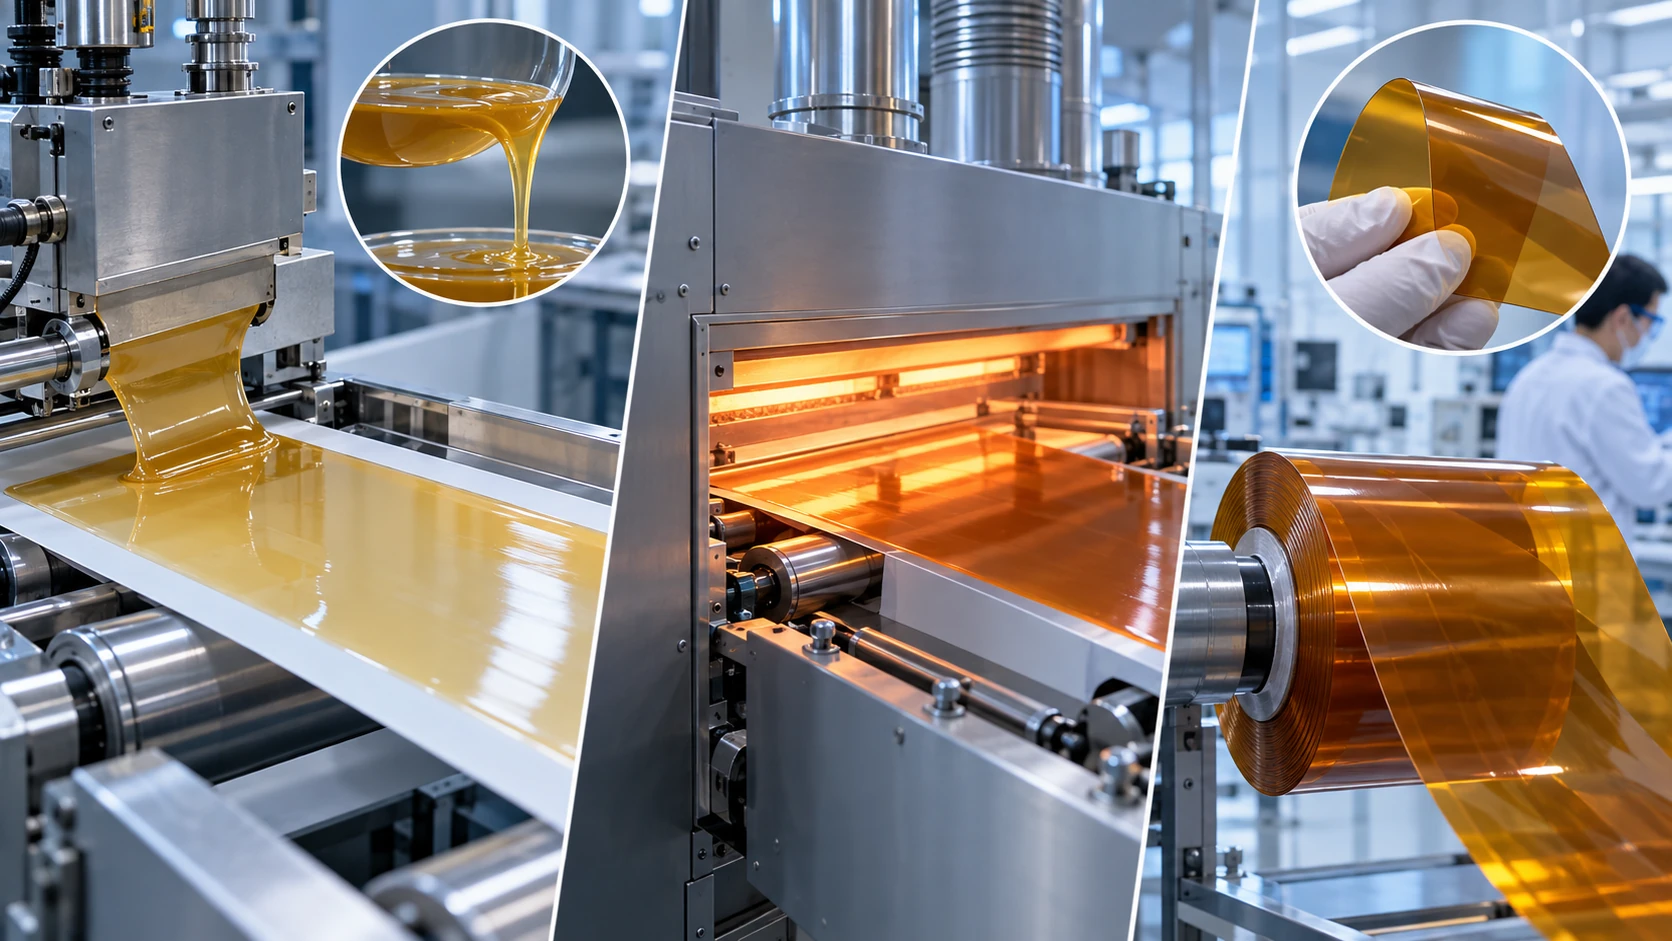
ImageGen conceptual illustration (not a real photograph or measurement). See the original diagram for exact values, names and structure.
Show original diagram with exact annotations and values
US Patent 3,179,614 (Edwards, DuPont; filed in 1961, published in 1965) states that reacting pyromellitic dianhydride and similar compounds with an aromatic diamine gives a "polyamic acid" that can be shaped, and that this can be converted into polyimide by heat treatment or chemical treatmentSourced. A related patent, US 3,179,634, names this two-stage route as the preferred method: react the diamine and the dianhydride in an organic solvent to make a polyamic acid intermediate, then heat it or treat it with a dehydrating agent to obtain the polyimideSourced.
The 2017 paper by Hasegawa et al. likewise calls this flow the conventional two-step process (casting of the precursor followed by thermal imidization)Sourced. According to the paper, there are three ways to make a film.
| Method | Flow | What the paper says |
|---|---|---|
| Two-step (thermal imidization) | Cast the polyamic acid onto a substrate and heat it to close the rings | For insoluble polyimide systems this is the only option. Thermal imidization takes place at 300 to 350 °C or above |
| Chemical imidization | Add a dehydrating agent (acetic anhydride and pyridine) to the polyamic acid solution, isolate the polyimide, redissolve it, then coat and dry | Usable only for highly soluble systems. Coating and drying take place at 250 °C or below |
| One-pot method | Reflux a monomer solution so that it becomes polyimide while still in solution | The simplest route, but the polymerization conditions have to be optimized |
All Sourced (Hasegawa et al., Polymers 2017, 9, 520 [Reference 6]).
The chemistry of Kapton can be read from how the standard is written
The DuPont datasheet states that Kapton HN meets the requirements of ASTM D5213, Type 1, item ASourced. ASTM D5213 (a specification for polymeric resin film for electrical insulation and dielectric applications) lists, as material (A), poly(N,N'-p,p'-oxydiphenylene pyromellitimide)Sourced. So Kapton HN corresponds to the polyimide made from pyromellitic dianhydride (PMDA) and 4,4'-oxydianiline (ODA) (this is our reading, linking an item in the standard to the datasheet statement).
UBE's UPILEX is described as made from BPDA (biphenyltetracarboxylic dianhydride), which the company produces itselfSourced. The company's material does not name the diamine component, so this article does not either.
3. A materials engineer's view (1): "it does not dissolve," so you build it from a precursor
With a thermoplastic you melt it, form it and cool it to harden it. Polyimide cannot be handled that way, so the stage where the shape is decided (a polyamic acid solution) and the stage where the properties are set (after ring closure) are separate. For a materials engineer that has three consequences (our commentary).
- The solvent leaves a mark on the final properties: the paper reports that, in the two-step thermal imidization process, the degree of film colouring increases in the solvent order HMPA ≫ NMP > DMAc ≥ GBL, triglyme (an empirical rule from that paper, for systems that would otherwise be colourless)Sourced. The suggested reason is that the solvent's boiling point and its interaction with the polymer change how long it stays in the film.
- The rings close while the film is held on a substrate: the same paper explains that if the film is fixed to its substrate during thermal imidization, the main chains line up in the plane of the film (in-plane orientation), which leads to a low coefficient of thermal expansion (CTE)Sourced. In other words, low CTE is a property built in by the process as well as by molecular design.
- Residual stress shows up as shrinkage on first heating: the DuPont datasheet states that residual stress put into the film during manufacture makes it shrink on its first exposure to elevated temperatureSourced. Before measuring the CTE, the paper recommends annealing the film in a free state at a temperature above the final heating temperature to remove residual stressSourced.
In handling precautions, the UBE catalog notes that the film contains a trace of DMAC and produces carbon monoxide above 300 °C, and calls for ventilationSourced. How solvents and by-products are handled bears directly on the design of high-temperature products and on safety on the shop floor.
4. The numbers: Kapton HN and UPILEX-S (manufacturers' stated values)
This section sets out values the manufacturers themselves publish for two representative polyimide films. The two are different products with different raw materials and different manufacturing methods, and neither the thickness nor the test conditions are the same. The table is not a ranking. It is there to show which items are reported, and by which test methods.
| Item | Kapton HN (manufacturer's stated value) | UPILEX-S (manufacturer's standard value) | Test method and conditions |
|---|---|---|---|
| Tensile strength | 231 MPa (23 °C) / 139 MPa (200 °C) | 520 MPa (25S, 25 °C) / 290 MPa (25S, 300 °C) | ASTM D882. Kapton: D-882-91 Method A, same value for 25 to 125 µm film thickness |
| Tensile modulus | 2.5 GPa (23 °C) / 2.0 GPa (200 °C) | 9.1 GPa (25S, 25 °C) / 3.7 GPa (25S, 300 °C) | ASTM D882 |
| Elongation at break | 72% (25 µm, 23 °C), 82% (50 to 125 µm, 23 °C), 83% (all thicknesses, 200 °C) | 40% (25S, 25 °C), 70% (25S, 300 °C) | ASTM D882 |
| Density | 1.42 g/cm³ | 1.47 g/cm³ | ASTM D1505 |
| Melting point | None | None | Kapton: ASTM E794. UPILEX: no test method stated |
| Heat shrinkage | 0.17% (150 °C, 30 min) / 1.25% (400 °C, 120 min) | 0.05% (25S, 200 °C, 2 h) | Kapton: IPC-TM-650 2.2.4A / ASTM D5214. UPILEX: ASTM D1204 |
| Dielectric constant (1 kHz) | 3.4 (25 µm, 23 °C, 50% RH) | 3.5 (25S, 25 °C) | ASTM D150 |
| Water absorption | (not confirmed in this article) | 1.4% (23 °C, 24 h immersion) / 0.8% (50 °C, 60% RH equilibrium) | UPILEX: ASTM D570 |
| Flame retardancy | UL94 V-0 | UL94 V-0 (table). The text also mentions VTM-0 | UL 94 |
Kapton HN: Qnity product page [Reference 1] and DuPont datasheet, December 2016 edition [Reference 2]. UPILEX-S: UBE catalog, April 2022 edition [Reference 3]. All Sourced (manufacturer's stated values).
Even when two entries both say "ASTM D882," the value changes with specimen dimensions, grip arrangement and test speed. ASTM D882 itself says that tensile properties vary with specimen thickness, method of preparation, test speed, grips and the way elongation is measured, so these must be matched strictly when comparingSourced [Reference 11]. The DuPont datasheet gives the specimen as 25 × 150 mm, with a grip separation of 100 mm and a speed of 50 mm/min. The UBE catalog does not state conditions of this kind. The edition of D882 cited here (D-882-91) is also an old one and differs from the current version.
As Fig. 2 shows, the linear expansion coefficient of Kapton HN rises with temperature (17 → 32 → 40 → 44 ppm/°C). Meanwhile Qnity's product page gives 20 ppm/°C (50 to 200 °C, JIS K 7197), and Table 2 of the 2016 datasheet gives 20 ppm/°C (−14 to 38 °C, ASTM D696)Sourced. The same "20" thus comes with a different temperature range, a different test method and a different thermal history. JIS K 7197 is the Japanese standard test method for the linear expansion of plastics by thermomechanical analysis (TMA) [Reference 12].
5. Our calculation: thermal expansion and the shrinkage on first heating
Using the datasheet's interval-by-interval coefficients, we work out the expansion on heating from 30 °C to 400 °C and check it against the overall value (34 ppm/°C)Our calculation.
- 30 to 100 °C: 70 K × 17 ppm/°C = 1,190 ppm
- 100 to 200 °C: 100 K × 32 ppm/°C = 3,200 ppm
- 200 to 300 °C: 100 K × 40 ppm/°C = 4,000 ppm
- 300 to 400 °C: 100 K × 44 ppm/°C = 4,400 ppm
- Total = 12,790 ppm = about 1.28% (about 1.28 mm on a length of 100 mm)
- Using the overall value instead: 370 K × 34 ppm/°C = 12,580 ppm = about 1.26% (about 1.26 mm per 100 mm). The difference is about 1.7%
Comparison with the shrinkage on first heating: the datasheet gives a heat shrinkage of 1.25% (400 °C, 120 min). That is almost the same size as the reversible thermal expansion above (about 1.26 to 1.28%).
Assumptions and limits: the interval coefficients are for a 25 µm film that has been given a thermal history, and the agreement with the overall value shows only that the datasheet's numbers are consistent with one another. The 1.25% shrinkage is a value for one specific condition, 400 °C for 120 minutes, and the datasheet row gives no specimen size or thickness. Expansion and shrinkage should not be added or subtracted to predict an actual dimensional change.
A thermal expansion coefficient describes an amount that goes back when the temperature returns. Shrinkage on first heating does not go back. For applications such as flexible-circuit wiring, where fine conductors are built on the film, the film has to be taken through a heat cycle once before the wiring is made, to let its dimensions settle (or the design has to allow for the shrinkage from the start) (our commentary). A low expansion coefficient on its own does not reveal this problem. We cover how to read thermal expansion coefficients in our explainer on the coefficient of thermal expansion.
6. A materials engineer's view (2): what it means to have no glass transition point
The DuPont datasheet describes the glass transition of Kapton as follows: A second order transition occurs in Kapton between 360 °C and 410 °C and is assumed to be the glass transition temperature. Different measurement techniques produce different results within that temperature rangeSourced. The melting point in the same datasheet is "None".
This article splits "high heat resistance" into three (commentary).
| Yardstick | What it looks at | Values that appear in this article (manufacturers' stated values, papers) |
|---|---|---|
| Short-term heat resistance | When softening or decomposition begins (Tg, melting point, weight loss) | Kapton second-order transition at 360 to 410 °C (depends on the measurement technique). Neopulim S100 / S200: Tg 308 / 327 °C (TMA), 1% weight-loss temperature 473 / 483 °C (TGA) |
| Long-term heat resistance | How long the material lasts in continuous use before a property falls below an allowable level (RTI, thermal life) | Kapton HN: UL RTI 240 °C electrical, 200 °C mechanical strength (UL 746B). UPILEX-25S: thermal life for tensile strength of 20,000 hours at 290 °C (constant-temperature method) |
| Dimensional stability | The amount the material expands and contracts with heat and does not return (CTE, heat shrinkage) | See Sections 4 and 5 |
A high Tg and a long service life are different things. And a modulus that does not fall much even above Tg (no clear Tg visible in dynamic mechanical analysis) is regarded as ideal for a substrate material. As a target for plastic substrates, Hasegawa et al. give a Tg realistically above 350 °C and, ideally, above 400 °C, or no marked softening up to 400 °C (no clear Tg detected by DMA)Sourced.
How glass transition is measured (the differences between DSC, TMA and DMA), and how to think about creep and stress relaxation, are covered in our explainer on the glass transition and creep.
7. Polyimide inside flexible printed circuits (FPC)
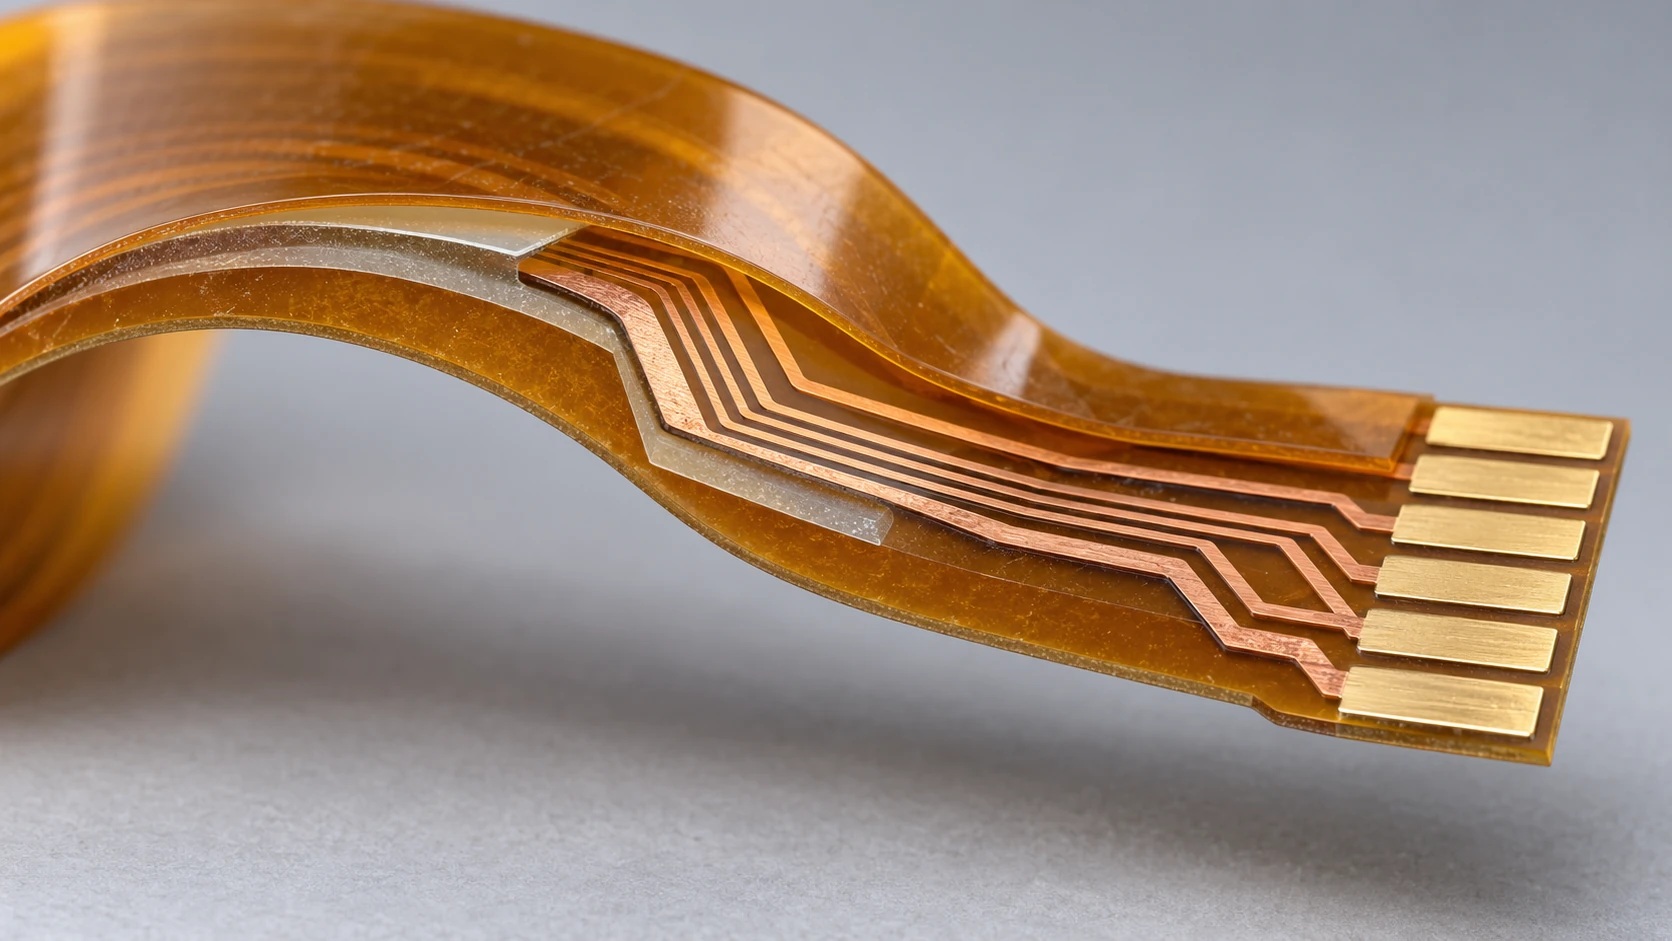
ImageGen conceptual illustration (not a real photograph or measurement). See the original diagram for exact values, names and structure.
Show original diagram with exact annotations and values
A technical article from Sumitomo Electric Industries (SEI Technical Review No. 172, 2008) describes the FPC as followsSourced.
- Structure: in a single-sided FPC, the circuit is made by etching the copper foil in the middle, and polyimide film insulating layers are bonded above and below it with a thermosetting adhesive to protect it from external stress. To meet demands for heat resistance and thinness, adhesive-free two-layer base materials are also widely used.
- Why polyimide: the insulating layer is generally a PI film with excellent heat resistance and a thermal expansion coefficient close to that of copper foil. PET is sometimes used where heat-resistance requirements are low, and liquid crystal polymer (LCP) where high-frequency performance matters.
- What heat resistance means here: because FPCs have excellent heat resistance, components can be mounted by reflow soldering (heated solder treatment).
- Materials: the main PI film thicknesses are 25 µm (1 mil) and 12.5 µm (1/2 mil). Copper foil is either electrodeposited or rolled, and rolled copper foil is used when folding endurance is needed.
"A thermal expansion coefficient close to that of copper foil" is among the selection criteria for an FPC's insulating film because if the two bonded layers expand and contract differently, the result is warpage or delamination. We discuss the stress that a mismatch in expansion coefficient puts on components and layers in our explainer on the coefficient of thermal expansion. The other criterion is flex durability. In the MIT folding endurance test (ASTM D2176), the datasheet shows Kapton HN surviving 285,000 cycles at 25 µm but 5,000 cycles at 125 µm, so the thicker the film, the fewer the cyclesSourced (manufacturer's stated value, DuPont datasheet). It makes sense, even for the same material, to use thin film for moving parts (our commentary).
The classification and quality requirements of metal-clad laminates for FPCs are set out in IPC-4204 (flexible metal-clad dielectrics for use in the fabrication of flexible printed boards). According to the standard's description on the ANSI webstore (IPC-4204B-2018), it covers materials with polyester, polyimide or liquid crystal polymer as the dielectricSourced [Reference 13].
8. Polyimide in semiconductors and lithium-ion batteries
Semiconductors: insulating films in the redistribution layer (RDL)
In semiconductor back-end processing, polyimide is also used as an insulating film made photosensitive, so that it can be patterned by exposure and development. We cover this use in detail in our explainer on the RDL, so we do not repeat it here. That explainer sets out the properties of photosensitive polyimide and PBO (polybenzoxazole), and the move to low-temperature curing, based on manufacturers' published material. From the point of view of two-step synthesis, some products form the pattern at the precursor stage and then close the rings, while others use an already-imidized soluble varnish (not every photosensitive polyimide is of the precursor type). The issues where back-end resins overlap (Tg, CTE, warpage) are covered in our explainers on the coefficient of thermal expansion, underfill and molding compounds.
Lithium-ion batteries: a binder for silicon anodes
A paper in the journal Nanomaterials (2021) says the following about silicon anodesSourced [Reference 9].
- Silicon has a theoretical capacity about ten times that of graphite, but lithiation causes a volume change of up to about 300%. Under repeated charge and discharge the active material cracks or peels off the current collector, and cycling performance falls.
- The PVDF binder common in graphite anodes is said to be unable to withstand the mechanical stress of a silicon anode.
- Starting from the idea of using polyimide as a binder, the authors synthesized a water-soluble polyamic acid salt (W-PAmAS) and made silicon electrodes with a low-temperature treatment at 150 °C. Introducing carboxylic acid groups raised adhesion, and the authors report a capacity of 2061 mAh/g and 1883 mAh/g after 200 cycles at 1200 mA/g (a laboratory-scale result).
What deserves attention in this study is that turning the polyamic acid into a salt makes it water-soluble, which avoids organic solvents, and that the ring-closing temperature is brought down to 150 °C so that the polymer can be used on an electrode. Given that polyimide is normally made by closing rings at high temperature, the design changes the precursor chemistry in order to change the process temperature and solvent (our commentary). On the other hand, this paper is a laboratory-scale report and does not show adoption in mass-produced batteries. Within the scope of this article, we could not confirm from primary sources any track record of mass-produced silicon-based batteries using a polyimide binder.
9. Transparent polyimide: why it is coloured, and the road to foldable displays
The paper by Hasegawa et al. summarizes the properties required of a heat-resistant plastic substrate for displays as followsSourced.
- To replace today's glass substrates (400 to 700 µm thick), plastic substrates thinner than 50 µm are wanted, for lighter, thinner and tougher displays.
- Meeting transparency, heat resistance, dimensional stability, film ductility and compatibility with the film-deposition process all at once is difficult, and the paper says that as of 2017 there was no reliable plastic substrate material.
- Commercial transparent super-engineering plastics (for example polyethersulfone, Tg 225 °C) do not have enough short-term heat resistance.
- Example targets: a Tg above 350 °C (ideally above 400 °C), an in-plane linear expansion coefficient below 10 ppm/K (ordinary polymers: 50 to 120 ppm/K), and, for a 20 to 30 µm film, yellowness index YI < 3 and haze < 1.0%.
Another paper, aimed at foldable displays (Micromachines 2021), reports research on using a hard-coated film on a colourless polyimide (CPI) substrate as the cover window of flexible and foldable displaysSourced [Reference 10]. A film that replaces cover glass needs high transmittance, resistance to bending, scratch resistance and protection against impact.
ImageGen conceptual illustration (not a real photograph or measurement). See the original diagram for exact values, names and structure.
Show original diagram with exact annotations and values
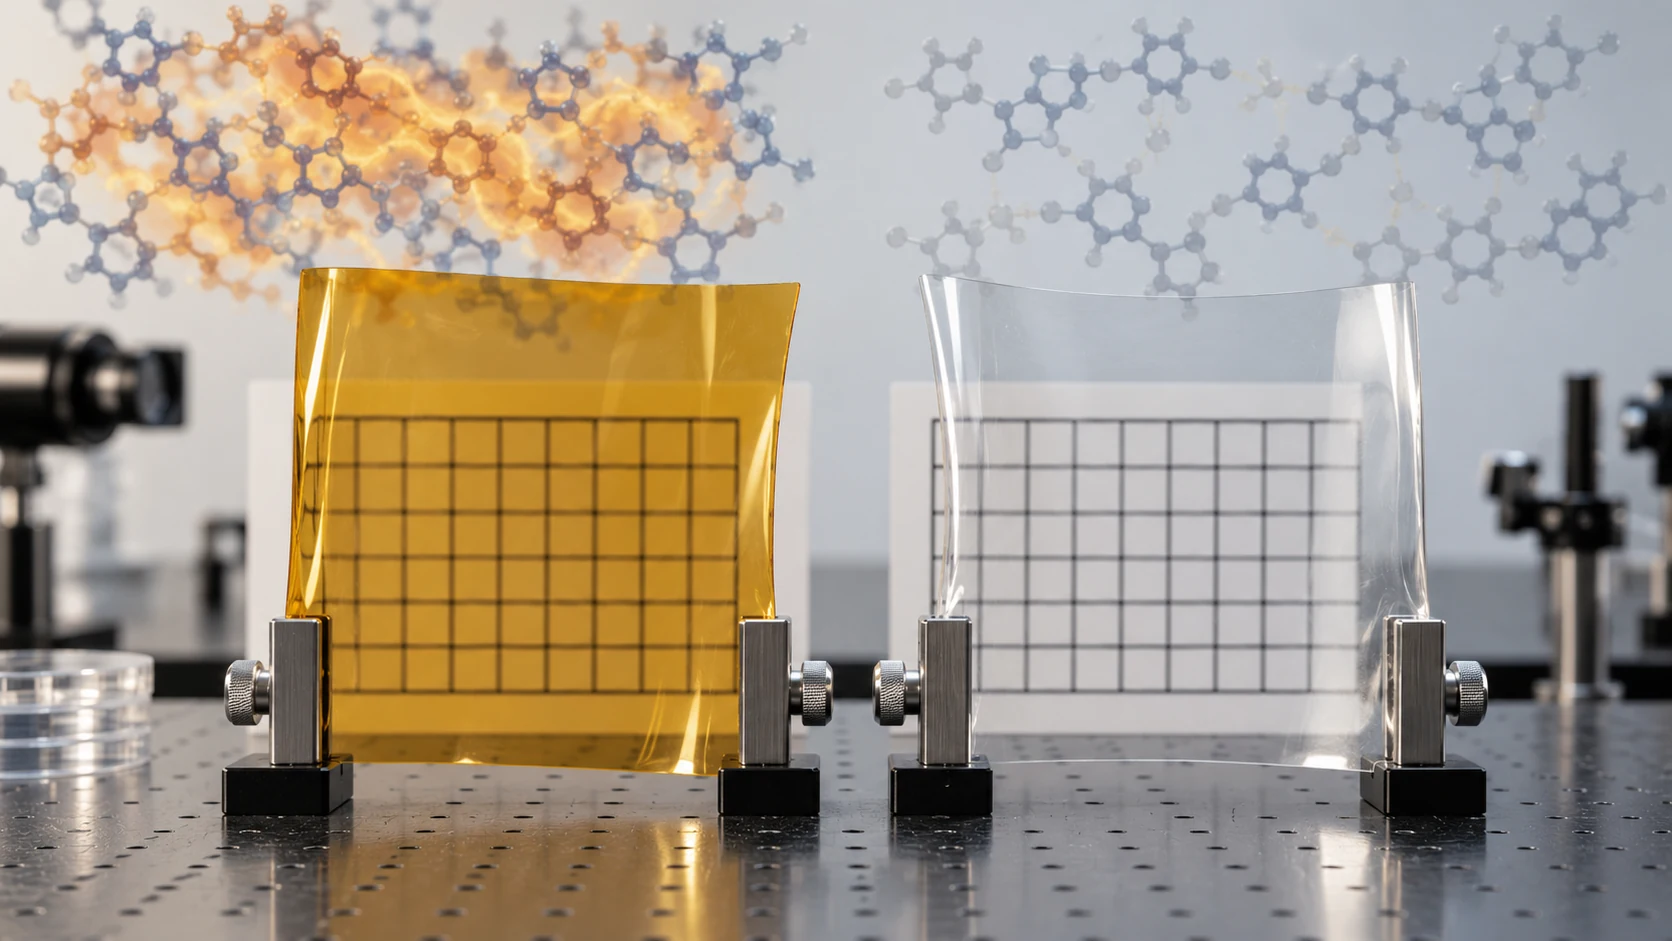
Why ordinary polyimide is yellow
Hasegawa et al. regard the main chain of a fully aromatic polyimide as an alternating sequence of electron donors (the N-aromatic part) and electron acceptors (the diimide part). Intramolecular and intermolecular donor-acceptor charge-transfer (CT) interactions create a new absorption band in the visible range that the original components do not have, and this is held to be the cause of the colour of aromatic polyimide filmsSourced. The paper gives a 15 µm UPILEX-S film, with a yellowness index of YI = 46.0, as an exampleSourced.
Besides CT interactions, coloration also involves decomposition of terminal amino groups, aliphatic parts of the main chain, aggregation of the chains (affected by the imidization method and heating programme), and process factors such as temperature, atmosphere and solventSourced. That colour is "not decided by polymer design alone" is an important point on the shop floor.
Published values for commercial transparent polyimide varnish
Mitsubishi Gas Chemical's Neopulim is described as a transparent polyimide varnish that is already imidized and soluble in solvents, which becomes a film simply when the solvent evaporates. The standard grades S100 and S200 are described as containing no fluorine at all (PFAS-free)Sourced.
| Item | Neopulim S100 | Neopulim S200 | Conditions (manufacturer's stated) |
|---|---|---|---|
| Glass transition temperature Tg | 308 °C | 327 °C | TMA |
| 1% weight-loss temperature | 473 °C | 483 °C | TGA |
| Total light transmittance | 89.9% | 90.4% | 50 µm film thickness (as given on the company's page) |
| Linear expansion coefficient | 66 ppm/K | 57 ppm/K | 100 to 200 °C |
| Yellowness index YI | 1.5 | 1.3 | 50 µm film thickness (as given on the company's page) |
All Sourced (Mitsubishi Gas Chemical Neopulim product page [Reference 7], manufacturer's stated values).
10. A materials engineer's view (3): what do you lose by making it transparent?
As Fig. 6 shows, Neopulim's linear expansion coefficient (57 to 66 ppm/K at 100 to 200 °C) is larger than the published values for coloured polyimide films (20 ppm/°C for Kapton HN at 50 to 200 °C; 12 ppm/°C for UPILEX-25S at 50 to 200 °C), and does not reach the target of below 10 ppm/K set by Hasegawa et al. Because the measurement conditions differ, this size comparison cannot rank the materials. Even so, the tendency for thermal expansion to grow as a film is made transparent is consistent with the difficulty the paper itself describes, that transparency and low CTE are hard to combine (our commentary).
The reason can be read from the molecular structure. The paper explains that low CTE requires monomers with a linear, rigid structure, and that the chains this produces tend to line up in the plane of the film (in-plane orientation)Sourced. Making the film transparent, on the other hand, requires weakening the donor-acceptor interaction, and putting in other structures to do so brings other problems. The paper gives three examplesSourced.
- 6FDA systems: a "hinge" formed by the hexafluoroisopropylidene group twists the imide part and destroys the linearity of the main chain, so a thermally imidized 6FDA/TFMB film does not reach a low CTE.
- Alicyclic diamine (t-CHDA): a strong salt forms early in the polymerization, so the reaction stalls or takes a long time. The s-BPDA / t-CHDA system gives a film with about 80% transmittance at 400 nm, a Tg above 300 °C and a CTE of 10 ppm/K, but a maximum elongation at break of only about 10%, so it is somewhat brittle.
- Alicyclic dianhydride (CBDA): suited to low CTE, but most of these polymers do not dissolve in common organic solvents, so solution processing is impossible. In addition the ring opens easily with moisture, and imidization needs a higher temperature.
The same paper also reports that, in its systems, films made by chemical imidization are more transparent and have a lower CTE than films made by the conventional two-step processSourced.
In short, transparent polyimide design involves five properties: transparency, heat resistance (high Tg), low CTE, toughness and solution processability. Getting one makes another harder. For a materials engineer it is a multi-objective optimization problem, closer to alloy design for metals and ceramics or to glass composition design (our commentary).
11. Challenges and limits
- The trade-off between heat resistance and processability: the more rigid and insoluble the structure, the higher the heat resistance and the harder the processing. Soluble polyimides are easier to process but give up something in Tg and CTE.
- Shrinkage on first heating, and dimensional control: residual stress from manufacturing appears as shrinkage on first heating. Precision circuits need heat treatment beforehand or an allowance in the design.
- Solvents and environmental regulation: two-step synthesis depends on polar solvents such as DMAc and NMP. Alongside handling safety (for example, carbon monoxide at high temperature), regulatory trends need to be checked (this article does not assess individual regulations).
- The multi-objective trade-off of transparency: as Section 10 showed, it is hard to achieve transparency together with low CTE, high Tg and toughness.
- Issues specific to cover windows: surface hardness (hard coat), fold marks and changes in appearance after repeated folding are matters of the laminate structure as well as of the film material itself. This article does not cover adoption in mass-produced foldable displays or market size, because we could not confirm them from primary sources.
- Recycling and disposal: most aromatic polyimides do not melt, so recycling by melting and reforming is probably poorly suited to them (our commentary). Within the scope of this article, we could not confirm primary-source information on chemical recycling or incineration.
12. Glossary
- Polyimide
- A polymer with imide rings in its main chain. Aromatic types have high heat resistance, and most neither melt nor dissolve readily.
- Polyamic acid
- The precursor formed first from a diamine and a dianhydride. It dissolves in organic solvents and, after shaping, closes its rings to become polyimide.
- Imidization (ring closure)
- The reaction in which polyamic acid loses water and forms imide rings. It proceeds with heat or with chemical treatment.
- PMDA / ODA
- Pyromellitic dianhydride / 4,4'-oxydianiline. The combination that corresponds to Kapton (read from the wording of the standard).
- BPDA
- Biphenyltetracarboxylic dianhydride. The raw material of UBE's UPILEX.
- Charge-transfer (CT) interaction
- An interaction between a part that gives up electrons and a part that takes them up. The cause of the colour of aromatic polyimide.
- Yellowness index (YI)
- A measure of how yellow a film is. The smaller the value, the closer to colourless.
- TMA
- Thermomechanical analysis. It measures the dimensional change of a specimen as temperature rises, giving the linear expansion coefficient and Tg.
- DMA
- Dynamic mechanical analysis. It measures how the modulus changes as temperature rises, and is used to find Tg.
- RTI
- Relative thermal index. An indicator in UL 746B of the temperature at which a material can be used over a long period.
- FPC
- Flexible printed circuit. A wiring board with copper circuits on a flexible insulating film.
- CPI
- Colourless polyimide. Used in research on items such as the cover of foldable displays.
13. References
- Qnity Electronics (formerly the electronics business of DuPont) "Kapton® HN Polyimide Film" product page — https://www.qnityelectronics.com/kapton-hn.html
- DuPont "DuPont™ Kapton® HN Polyimide Film" datasheet K-15345-2 (December 2016 edition). A copy hosted on a distributor's site — https://www.epectec.com/downloads/DuPont-Kapton-HN-Polyimide-Film.pdf
- UBE "UPILEX®-S" catalog (April 2022 edition, PDF) — https://ube.com/upilex/catalog/pdf/upilex_s_e.pdf
- W. M. Edwards (E. I. du Pont de Nemours) US 3,179,614 "Polyamide-acids, compositions thereof, and process for their preparation" (published 1965) — https://patents.google.com/patent/US3179614A/en
- W. M. Edwards (E. I. du Pont de Nemours) US 3,179,634 "Aromatic polyimides and the process for preparing them" (published 1965) — https://patents.google.com/patent/US3179634A/en
- M. Hasegawa "Development of Solution-Processable, Optically Transparent Polyimides with Ultra-Low Linear Coefficients of Thermal Expansion", Polymers 2017, 9(10), 520 (DOI: 10.3390/polym9100520, open access) — https://pmc.ncbi.nlm.nih.gov/articles/PMC6418549/
- Mitsubishi Gas Chemical Company "Neopulim™ (Transparent polyimide varnish)" product page — https://www.mgc.co.jp/eng/products/ac/neopulim.html
- Sumitomo Electric Industries Masayuki Kanehiro et al., "FPC Business of Sumitomo Electric", SEI Technical Review No. 172 (January 2008, PDF; the body text is in Japanese) — https://sei.co.jp/technology/tr/bn172/pdf/sei10521.pdf
- Nanomaterials 2021, 11(12), 3164 "Eco-Friendly Water-Processable Polyimide Binders with High Adhesion to Silicon Anodes for Lithium-Ion Batteries" (DOI: 10.3390/nano11123164, open access) — https://pmc.ncbi.nlm.nih.gov/articles/PMC8705944/
- Micromachines 2021, 12(3), 233 "Transparent and Flexible SiOC Films on Colorless Polyimide Substrate for Flexible Cover Window" (DOI: 10.3390/mi12030233, open access) — https://pmc.ncbi.nlm.nih.gov/articles/PMC7996484/
- ASTM International "ASTM D882-18 Standard Test Method for Tensile Properties of Thin Plastic Sheeting" (listed as a historical version) — https://store.astm.org/d0882-18.html
- National Institute of Advanced Industrial Science and Technology (AIST) "Thermal expansion: standards and measurement-standard information" (a list including JIS K 7197:2012; in Japanese) — https://unit.aist.go.jp/mcml/rg-tp/research/1/index-3.html
- IPC / ANSI Webstore "IPC 4204B-2018 Flexible Metal-Clad Dielectrics For Use In Fabrication Of Flexible Printed Boards" (listed as a historical version) — https://webstore.ansi.org/standards/ipc/ipc4204b2018
- ASTM International "ASTM D5213-19 Standard Specification for Polymeric Resin Film for Electrical Insulation and Dielectric Applications" — https://store.astm.org/d5213-19.html
14. Claim-to-source audit
| Claim in the text | Basis | Label |
|---|---|---|
| That Kapton HN is a general-purpose film that has been used from −269 °C to 400 °C; density 1.42 g/cm³ (ASTM D1505), thermal conductivity 0.20 W/m·K (ASTM D5470), linear expansion coefficient 20 ppm/°C (50 to 200 °C, JIS K 7197), UL RTI 240 °C electrical and 200 °C mechanical strength (UL 746B), UL94 V-0, tensile strength 231.0 MPa (23 °C, ASTM D882), and its applications | Qnity product pageReference 1 https://www.qnityelectronics.com/kapton-hn.html | Sourced |
| Kapton HN tensile strength 231 / 139 MPa, modulus 2.5 / 2.0 GPa, elongation at break 72% (25 µm) and 82% (50 to 125 µm) at 23 °C and 83% at 200 °C, density, MIT folding endurance (285,000 cycles at 25 µm, 5,000 cycles at 125 µm, ASTM D2176), no melting point (ASTM E794), 20 ppm/°C at −14 to 38 °C (ASTM D696), interval CTEs (17, 32, 40, 44 and 34 ppm/°C), heat shrinkage 0.17% and 1.25%, dielectric constant 3.4, a second-order transition at 360 to 410 °C that depends on measurement technique, shrinkage on first heating, specimen dimensions, and conformity to ASTM D5213 type 1 item A | DuPont Kapton HN datasheet K-15345-2Reference 2 https://www.epectec.com/downloads/DuPont-Kapton-HN-Polyimide-Film.pdf | Sourced |
| That UPILEX is made from BPDA; UPILEX-S tensile strength, modulus and elongation (25S: 520 MPa, 9.1 GPa and 40% at 25 °C; 290 MPa, 3.7 GPa and 70% at 300 °C), linear thermal expansion coefficient (12, 16, 20 and 22 ppm/°C at 50 to 200 °C), heat shrinkage (0.05% at 200 °C for 2 h), no melting point, thermal life (tensile strength, 20,000 hours at 290 °C), water absorption, dielectric constant, density, and the caution about trace DMAC and carbon monoxide above 300 °C | UBE UPILEX-S catalogReference 3 https://ube.com/upilex/catalog/pdf/upilex_s_e.pdf | Sourced |
| The method of making a polyamic acid and converting it to polyimide by heat or chemical treatment after forming, and that pyromellitic dianhydride and an aromatic diamine give a polyamic acid | Edwards, US 3,179,614Reference 4 https://patents.google.com/patent/US3179614A/en | Sourced |
| That the two stages are reacting a diamine and a dianhydride in an organic solvent to make a polyamic acid intermediate, then heating or using a dehydrating agent to make polyimide | Edwards, US 3,179,634Reference 5 https://patents.google.com/patent/US3179634A/en | Sourced |
| The three routes: thermal imidization (300 to 350 °C or above), chemical imidization (coating and drying at 250 °C or below) and the one-pot method; the solvent order for coloration; in-plane orientation and low CTE; annealing to remove residual stress; the cause of coloration (CT interaction), YI = 46.0 (UPILEX-S, 15 µm), substrate targets (Tg above 350 to 400 °C, CTE below 10 ppm/K, YI < 3, haze < 1.0%); s-BPDA/t-CHDA (T400 about 80%, Tg above 300 °C, CTE 10 ppm/K, elongation at break about 10%), CBDA(70);6FDA(30)/AB-TFMB (CTE 7.3 ppm/K, T400 = 80.6%, YI = 2.5, Tg = 329 °C); and the problems of 6FDA systems, t-CHDA and CBDA | Hasegawa, Polymers 2017Reference 6 https://pmc.ncbi.nlm.nih.gov/articles/PMC6418549/ | Sourced |
| That Neopulim is a soluble, already-imidized varnish; S100 / S200 Tg of 308 / 327 °C (TMA), 1% weight-loss temperature of 473 / 483 °C, total light transmittance of 89.9 / 90.4%, linear expansion coefficient of 66 / 57 ppm/K (100 to 200 °C), YI of 1.5 / 1.3, 50 µm film thickness, and that it contains no fluorine | Mitsubishi Gas Chemical Neopulim product pageReference 7 https://www.mgc.co.jp/eng/products/ac/neopulim.html | Sourced |
| The structure of the FPC (single-sided, double-sided, multilayer; adhesive layer; coverlay opening), the conditions for PI film in the insulating layer (heat resistance, expansion coefficient close to copper), PI film thicknesses of 25 and 12.5 µm, copper foil types and thicknesses of 35, 18 and 12 µm, that reflow mounting is possible, the use of PET and LCP, and two-layer base materials | SEI Technical Review No. 172Reference 8 https://sei.co.jp/technology/tr/bn172/pdf/sei10521.pdf | Sourced |
| That the volume change of a silicon anode is up to about 300%, that PVDF is unsuitable, and that an electrode with a water-soluble polyamic acid salt binder treated at 150 °C gave 2061 mAh/g and 1883 mAh/g after 200 cycles at 1200 mA/g | Nanomaterials 2021Reference 9 https://pmc.ncbi.nlm.nih.gov/articles/PMC8705944/ | Sourced |
| That research exists on using a hard-coated film on a CPI substrate as the cover window of flexible and foldable displays, and the properties required of a cover-window film (transmittance, bending, scratch resistance, impact protection) | Micromachines 2021Reference 10 https://pmc.ncbi.nlm.nih.gov/articles/PMC7996484/ | Sourced |
| That ASTM D882 is the test method for tensile properties of thin plastic sheeting, and that because tensile properties vary with specimen thickness, preparation, speed, grips and the way elongation is measured, strict control is needed for comparison | ASTM D882-18 (Significance and Use 5.1)Reference 11 https://store.astm.org/d0882-18.html | Sourced |
| That JIS K 7197:2012 is the test method for the linear expansion of plastics by thermomechanical analysis | AIST standards information pageReference 12 https://unit.aist.go.jp/mcml/rg-tp/research/1/index-3.html | Sourced |
| That IPC-4204B-2018 sets the classification and quality requirements of metal-clad materials with polyester, polyimide or liquid crystal polymer as the dielectric | ANSI Webstore description of the standardReference 13 https://webstore.ansi.org/standards/ipc/ipc4204b2018 | Sourced |
| That ASTM D5213 is a specification for polymeric resin film for electrical insulation and dielectric applications, and that its material (A) is poly(N,N'-p,p'-oxydiphenylene pyromellitimide) | ASTM D5213-19Reference 14 https://store.astm.org/d5213-19.html | Sourced |
| That adding up the interval CTEs of Kapton HN gives about 12,790 ppm (about 1.28%), that the overall value of 34 ppm/°C gives 12,580 ppm (about 1.26%), a difference of about 1.7%, and that the 1.25% heat shrinkage at 400 °C for 120 min is about the same size as the reversible thermal expansion | Our calculation. The interval CTEs and heat shrinkage are datasheet values for 25 µm film after thermal exposure. The specimen size for the heat shrinkage was not confirmed, so the figure cannot be used to predict dimensional change | Our calculation |
| That the chemical composition of Kapton corresponds to the combination of PMDA and ODA | Commentary: our reading, linking the datasheet statement of conformity to ASTM D5213 type 1 item A with the name of material (A) in the standard. The composition is not stated directly in DuPont's material | Commentary |
| The three-yardstick breakdown of heat resistance, the design meaning of "it does not dissolve, so build it from a precursor," the reason for choosing thin film for FPCs, the reading that changing the precursor chemistry changes the process, the multi-objective trade-off of transparency, and how Figs. 1, 3 and 5 are drawn | Our summary and commentary based on published content. Not views expressed by the companies or institutions | Commentary |
| The diamine component of UPILEX-S, the water absorption of Kapton HN, and individual test-standard numbers in the Mitsubishi Gas Chemical material | Not stated, because they could not be confirmed from primary sources within the scope of this article | Commentary |
| Adoption of CPI in mass-produced foldable displays, a mass-production record for silicon-based batteries using polyimide binders, and polyimide recycling technology | Not stated, because they could not be confirmed from primary sources within the scope of this article (and not treated as future developments) | Not yet confirmed |
| That Figs. 2 and 6 are drawings of published values, and that Fig. 4 and the hero image are AI-generated images that do not show real products or experiments | Note by this article | Commentary |
Last updated 2 October 2026. Sources are limited to primary material (manufacturers' product pages, datasheets and catalogs, patents, peer-reviewed papers, and public information from standards bodies and industry associations). Property values are manufacturers' stated values or values from the literature, given with test method, conditions and source, and values for different products or conditions are not set side by side to rank them. The water absorption of Kapton HN, the diamine component of UPILEX-S, adoption in mass-produced foldable displays, a mass-production record for polyimide-binder silicon batteries, and polyimide recycling are not stated here because they could not be confirmed from primary sources. Figs. 1, 2, 3, 5 and 6 are vector drawings; the hero image and Fig. 4 are AI-generated images, and none of them shows a real micrograph or physical product.