TECHNOLOGY EXPLAINER
Atomic Layer Deposition (ALD)
— stack reactions that stop when saturated, and set thickness by counting
ALD builds a film by alternating two gases and repeating reactions that stop once the surface is saturated. The growth per cycle (GPC) is on the order of 0.1 nm, so thickness is set by the number of cycles, and even deep three-dimensional structures can be coated uniformly. The price is time: in a laboratory example where one cycle takes seconds, a 5 nm film takes more than half an hour. This article sets out the mechanism, precursors and reactants, thermal and plasma ALD, area-selective ALD, applications and the time problem, keeping the origin of each number clear.
- What atomic layer deposition (ALD) is (the short version)
- Self-limiting reactions and the cycle
- Thickness set by the number of cycles: the ALD window
- Precursors and reactants: what is combined, and how
- Thermal ALD and plasma ALD
- Coating three-dimensional structures
- Area-selective ALD
- Applications: high-k gate dielectrics, DRAM, spacers, barrier layers
- The throughput problem: our calculation
- How to read the numbers
- Limits / Glossary / References / Claim-to-source audit
Sourced = a statement in published material (link given)
Our calculation = a figure this article derived, with the assumptions spelled out
Not yet confirmed = a plan or target with no confirmed track record
Structural readings and materials-design interpretations are marked separately as Commentary.
Growth rates and film properties are written together with what was measured (method), which tool and conditions (temperature, pulses, substrate) and at what level (laboratory or production). Company statements are labelled as the manufacturer's, and market-size estimates by research firms are not used.
This is an explainer on the principles and evaluation of film deposition in semiconductor manufacturing. Precursors (gases and vapours) include toxic, pyrophoric and corrosive substances, and their handling is governed by the supplier's safety data sheets (SDS) and the law. This article gives no handling advice and does not rank any company, tool or country.
1. What atomic layer deposition (ALD) is (the short version)
ALD is a method that supplies two reactants to a surface in turn and builds a film in units close to an atomic layer, using the fact that each reaction saturates and stops on the surface. If etching is "removing", this is "stacking uniformly".
- Definition: Puurunen (a 2005 review) describes ALD as a chemical vapor deposition technique based on sequential self-terminating gas–solid reactions, used for about four decades to make conformal inorganic layers down to nanometre thicknessSourced
- Breadth of use: ASM International lists high-k metal gates, spacer dielectrics for patterning, MIM capacitors, gate spacers and high-aspect-ratio gap-fill, among others (the manufacturer's description)Sourced
- 2025 was the ramp year for GAA (gate-all-around): in its 2025 annual report ASM says the 3D structure of GAA and the need for tighter control call for additional ALD steps (the manufacturer's statement)Sourced
ALD sets thickness by counting cycles, so thickness can be controlled precisely, but that costs time. Al2O3 (TMA/water) grows at about 1.1 Å per cycle and TiN (TiCl4/NH3) at about 0.47 Å per cycle, both laboratory reportsSourced. On the laboratory tool of the latter, one cycle takes 19.5 s, so a 5 nm TiN film takes about 35 minutesOur calculation. Combining precision with speed is being worked on in both tools and materials.
In this series, our explainer on lithography and EUV touched on the spacer films of multiple patterning, and our explainer on resists and photomasks touched on dry resists (films made by deposition). ALD is what actually lays down such films. The next article, on etching, covers the other side: removing what ALD deposits.
2. Self-limiting reactions and the cycle
One ALD cycle has four steps: 1. precursor, 2. purge (remove the excess with inert gas), 3. reactant, 4. purge (Oviroh et al., ASM). The reaction in each step saturates on the reactive surface sites and goes no further, so supplying more does not make the film thicker. Oviroh et al. say ALD resembles CVD but differs in that precursor adsorption is self-limiting and precursor and reactant are introduced alternately and in sequenceSourced.
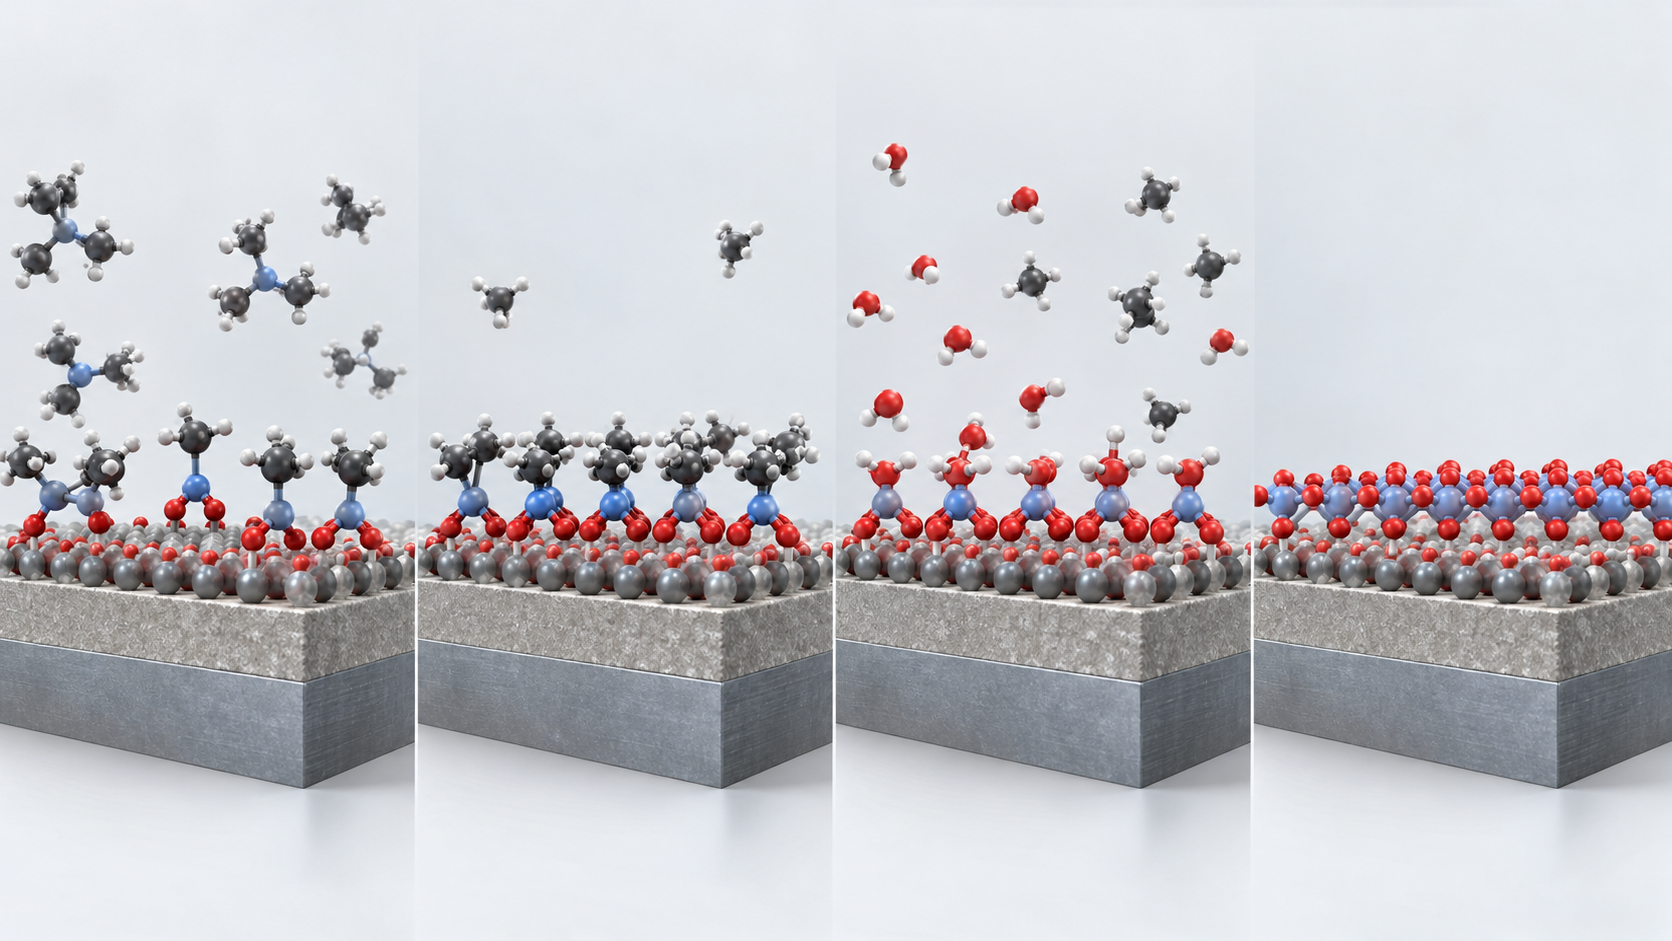
Shapes, colors and dimensions are illustrative. Consult the original schematic below for exact values and label correspondence.
View the original SVG schematic and exact annotations
Reading guide and original schematic labels: One ALD cycle: a self-limiting reaction repeated in four steps (conceptual) / Cross-section sketch. Molecule sizes and positions are schematic. / 1. Precursor pulse / Precursor (blue) / One layer adsorbs on the / reactive surface sites / 2. Purge / Exhaust / Excess precursor and / by-products are pumped out / 3. Reactant pulse / Reactant (red) / Reacts with the adsorbed / molecules to form film / 4. Purge / Exhaust / A new surface results; / on to the next cycle / Repeat steps 1 to 4 until the target thickness (N cycles) / * Self-limiting reaction and cycle: Puurunen's review [Source 1] and ASM's technical page [Source 8]. / * Sizes, coverage and growth per cycle (GPC) depend on the material; this is a conceptual diagram.
ALD assumes that the precursor does not meet the reactant in the gas phase and reacts only on the surface. If the purge is too short and precursor and reactant mix in the gas, CVD-like growth creeps in and the uniformity and conformality fall apart (this article's commentary). Also, the growth per cycle (GPC) is not "exactly one atomic layer"; it is a material-specific value set by the precursor's size (steric hindrance), the number of reactive sites and the temperature. Puurunen calls the trimethylaluminum (TMA) and water process for Al2O3 a "rather ideal ALD process" and uses it as the example for surface chemistrySourced. That such ideal processes are rather the minority is what makes developing ALD for new materials hard (commentary).
3. Thickness set by the number of cycles: the ALD window
Thickness = number of cycles × GPC (growth per cycle). The range in which GPC does not change with temperature or precursor amount is called the ALD window (Oviroh)Sourced.
Kim et al. (2022, peer-reviewed) grew Al2O3 from TMA and water in a traveling-wave-type ALD reactor (80 to 250 °C) and took the GPC from the slope of film thickness measured by spectroscopic ellipsometry against the number of cycles. GPC rose from about 0.9 Å per cycle at 80 °C to a constant about 1.1 Å per cycle at 150 °C and above, so 150 °C and above was the ALD window (purge time fixed at 40 s)Sourced. The authors attribute the lower GPC below 150 °C to a slower reaction caused by the thermal activation barrier for removing the ligand (CH3)Sourced.
Baishya et al. (2026, peer-reviewed) grew TiN from TiCl4 and NH3 at 400 °C. One cycle was a 0.5 s TiCl4 pulse, 4 s purge, 2.5 s NH3 pulse, 5 s purge, 2.5 s NH3 pulse and 5 s purge, giving about 0.047 nm per cycle. 100, 200, 300 and 400 cycles gave 4.7, 9.4, 14.1 and 18.8 nm (a laboratory ALD tool)Sourced.
From the laboratory GPC values, the number of cycles needed for a 10 nm filmOur calculation.
- Al2O3 (1.1 Å per cycle): 10 nm ÷ 0.11 nm = about 91 cycles
- TiN (0.047 nm per cycle): 10 nm ÷ 0.047 nm = about 213 cycles. The 4.7 nm TiN is 100 cycles
- Step of thickness: the thickness added per cycle is a guide to the smallest step (about 0.11 nm for Al2O3, about 0.047 nm for TiN)
Assumptions and limits: GPC changes with temperature, precursor, reactor and substrate state, and both values used here are laboratory-tool reports. The GPC of production tools, and cases where thickness is not proportional to cycles in early growth (nucleation), are not included.
4. Precursors and reactants: what is combined, and how
The film material is set by the combination of a precursor (the molecule that carries the metal or other element) and a reactant (a molecule or plasma that supplies oxygen, nitrogen and so on). Here are reported examples, with their conditions.
| Film | Precursor | Reactant | Conditions and measured values (level) | Source |
|---|---|---|---|---|
| Al2O3 | Trimethylaluminum (TMA) | Water | 80 to 250 °C. GPC about 0.9 Å (80 °C) and about 1.1 Å (150 °C and above). Spectroscopic ellipsometry (laboratory) | Kim et al. (2022) |
| HfO2 | Hafnium dimethylamide | Water | Fully conformal coverage of holes with aspect ratio 43 (laboratory) | Gordon et al. (2003) |
| TiN | TiCl4 (a chloride) | NH3 | 400 °C. About 0.047 nm per cycle (laboratory tool) | Baishya et al. (2026) |
| SiNx (thermal ALD) | Chlorosilane (e.g. Si2Cl6) | NH3 (or hydrazine) | Typically above 450 °C (review) | Meng et al. (2016) |
| SiNx (plasma ALD) | SiH4, trisilylamine, aminosilanes and others | N2, N2/H2 or NH3 plasma | Typically below 500 °C. Examples of 300 to 500 °C PEALD SiNx for spacers and similar in 32/28 nm HKMG are cited (review) | Meng et al. (2016) |
All Sourced (statements in the papers and reviews). Methods, tools and levels differ, so these are not a ranking of growth rates or temperatures.
A precursor must meet at least these conditions at once (this article's commentary): (1) enough vapour pressure to be delivered; (2) reactive with the surface at the reaction temperature but not decomposing at the supply temperature (this sets the upper edge of the ALD window); and (3) by-products that leave as gas and do not stay on the surface. The kind of ligand (chloride, organometallic) changes the impurities likely to remain. Kim et al. report that in Al2O3, the lower the growth temperature, the more carbon impurity and oxygen defects and the lower the dielectric breakdown strength. The film grown at 150 °C had a breakdown field of about 8.3 MV/cmSourced (measured under that paper's conditions; laboratory samples). Baishya et al. also report that ultrathin TiN oxidizes at the surface in air, and that the oxygen concentration measured by XPS is higher for thinner films (about 30% at 4.7 nm, about 18% at 18.8 nm). The authors explain that XPS probes the top 5 to 10 nm, so the oxidized layer weighs more in thin filmsSourced. So in evaluating ultrathin films, the film itself and the surface and interface layers must be considered separately.
From Baishya et al.'s four-point-probe sheet resistance (on glass, before exposure) and film thickness we calculate resistivity = sheet resistance × thicknessOur calculation.
- 100 cycles (4.7 nm): 222.3 kΩ/sq × 4.7 nm = about 100,000 µΩ·cm
- 200 cycles (9.4 nm): 2.5 kΩ/sq → about 2,350 µΩ·cm; 300 cycles (14.1 nm): 519 Ω/sq → about 730 µΩ·cm
- 400 cycles (18.8 nm): 287 Ω/sq → about 540 µΩ·cm (the same as the authors' value)
Assumptions and limits: the sheet resistance is the paper's value (glass substrate, before air exposure) and the thickness is the nominal one calculated from the growth rate. That the 4.7 nm value is about 200 times larger is consistent with continuity, surface oxidation and grain boundaries mattering more in thin films, but this article did not check the breakdown. The performance of TiN, used for barriers and electrodes, changes greatly with the thickness used.
5. Thermal ALD and plasma ALD
Thermal ALD drives the reaction with the heat of the substrate and chamber. Oviroh et al. say that thermal ALD proceeds only through surface reactions, so thickness control and conformality come easily regardless of substrate geometry and reactor design, but its typical temperatures are fairly high, 150 to 350 °CSourced. Plasma ALD (PEALD) uses a plasma in the reactant step to supply the reaction energy, which allows film growth at lower temperatures (ASM)Sourced.
| Item | Thermal ALD | Plasma ALD |
|---|---|---|
| Source of reaction energy | Heat of the substrate and chamber (Meng) | Radicals and ions in the plasma (Profijt, ASM) |
| Temperature | Typically 150 to 350 °C (Oviroh). SiNx above 450 °C (Meng) | Lower. SiNx typically below 500 °C (Meng) |
| Freedom in materials and precursors | Needs reactive precursors and reactants | A wider choice of precursors, reactants and material properties (Profijt) |
| Conformality | Good regardless of shape (Oviroh) | Can fall (Profijt). Radicals tend to recombine on walls in deep structures (Knoops et al.'s Monte Carlo work, introduced by Oviroh) |
| Other issues | High temperature can harm what lies beneath | Plasma damage (Profijt). More complex tools |
Sources: Oviroh et al. [Source 2], Profijt et al. [Source 7], Meng et al. [Source 4], ASM [Source 8]. "Needs reactive precursors and reactants" and "high temperature can harm what lies beneath" are this article's commentary.
ASM explains that PEALD enables low-thermal-budget applicationsSourced. What a transistor already has (dopant profiles, metals, low-k films, organic films) is sensitive to high temperature, so the later a film is laid down, the lower the temperature it needs (this article's commentary). The plasma, on the other hand, brings a trade-off between conformality and damage. Finding conditions that deposit at low temperature, uniformly into deep structures, and without damage is the heart of PEALD development (commentary).
6. Coating three-dimensional structures
One of ALD's greatest strengths is that it can coat evenly to the bottom of deep holes and trenches. Gordon et al. (2003, peer-reviewed) derived two conditions for uniform coating using self-limiting reactions: (1) a certain minimum amount of vapour must be supplied, and (2) a certain minimum product of vapour pressure and exposure time at the hole entrance. The theory agreed well with data in which HfO2 from hafnium dimethylamide and water coated holes of aspect ratio 43 completely conformallySourced.
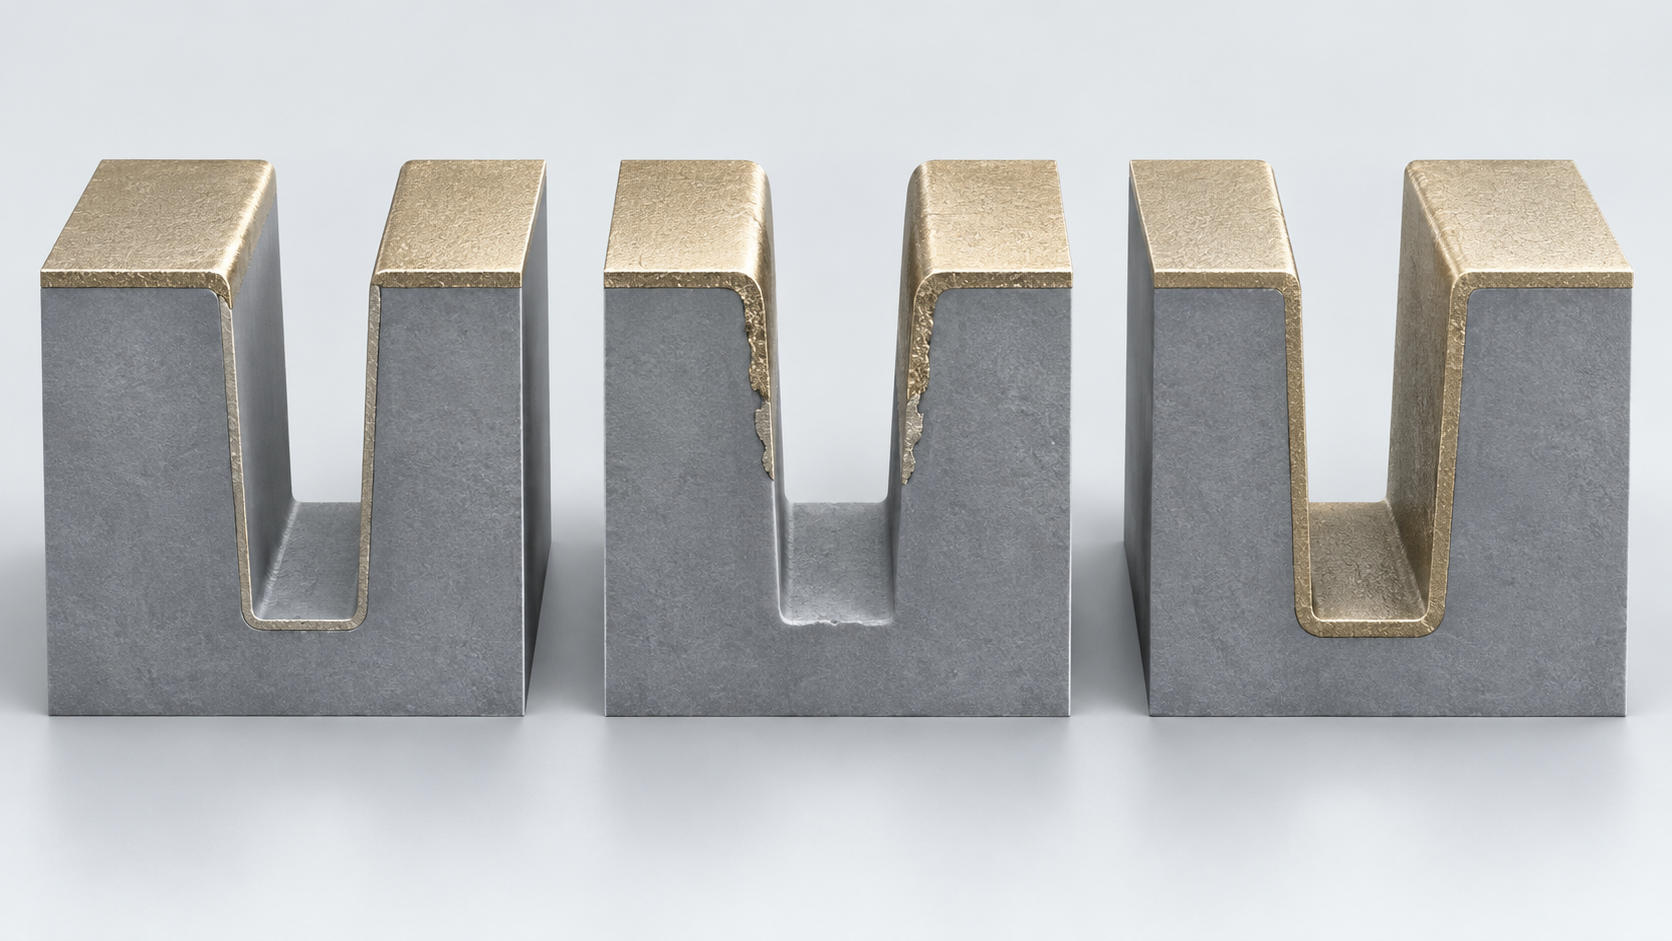
Shapes, colors and dimensions are illustrative. Consult the original schematic below for exact values and label correspondence.
View the original SVG schematic and exact annotations
Reading guide and original schematic labels: Coverage of steps and deep holes (conceptual) / Cross-section sketch. Orange is the deposited film. Differences in thickness are exaggerated. / Physical deposition (PVD) / Thick on top, thin on / sidewall and bottom / Chemical vapor deposition / In between; depends / on conditions / Atomic layer deposition / About the same thickness / on top, wall and bottom / Aspect ratio / width / depth / AR = depth ÷ width / deeper means harder to reach / * A concept of ALD's uniform coverage from self-limiting reactions [Sources 1, 8]; real thickness ratios are not shown. / * Gordon et al. [Source 6] report fully conformal HfO2 in holes of aspect ratio 43 using a hafnium amide and water.
The time for a precursor to diffuse to the bottom of a deep hole generally scales with the square of the depth (a basic diffusion relation; our assumption)Our calculation.
- If the aspect ratio doubles from 43 to 86, the guide to the required exposure is (86 ÷ 43)² = about 4 times
- From 43 to 100, (100 ÷ 43)² = about 5.4 times
Assumptions and limits: Gordon et al. say they derived "simple scaling laws", but this article did not check the equations themselves. The square law used here is a general guide to the time to diffuse in, and varies with the reaction probability (sticking) and how by-products escape. It shows the direction: deeper structures need longer exposure, which worsens the throughput problem discussed later.
7. Area-selective ALD
Area-selective ALD grows film only on a chosen material on the substrate. Mackus et al. (2019, peer-reviewed) say it is gaining momentum in semiconductor processing because of the growing need to eliminate the edge placement errors (EPE) of top-down processingSourced. This is continuous with the overlay-error problem we saw in our explainer on lithography and EUV.
The difficulty is keeping the selectivity. Mackus et al. say the general cause of lost selectivity is that the surface meant to stay free of film changes character while exposed to the ALD chemistry, and they point to correction steps such as surface functionalization or selective etching built into multistep cycles or "supercycles"Sourced. Rhee et al. (2025) likewise state that most studies showed loss of selectivity after a certain number of cycles; as an example they cite W growing only on hydrogen-terminated Si and not on hydroxyl-terminated SiSourced. ASM says its new XP8E platform supports advanced ALD and CVD applications, including selective deposition (the manufacturer's statement)Sourced.
That a correction step contains selective etching means ALD and etching become parts of one process rather than separate steps (this article's commentary). This is why atomic layer etching (ALE), covered in our explainer on etching, can serve as the correction for area-selective ALD. Also, selectivity exploits "the delay before nuclei form on the intended material", so it can generally be kept only while the film is thin (commentary). Selective deposition gets harder the thicker the film, so numbers should be read together with "selective up to how many cycles".
8. Applications: high-k gate dielectrics, DRAM, spacers, barrier layers
(1) High-k gate dielectrics and metal gates
Wilk et al. (2001, a peer-reviewed review) give the guidelines for choosing a gate dielectric to replace SiO2: permittivity, band gap and band alignment to silicon, thermodynamic stability, film morphology, interface quality, compatibility with CMOS processing, and reliabilitySourced. Mistry et al. (2007) report that a 45 nm logic technology for the first time incorporated high-k + metal-gate transistors in a volume manufacturing process, with a high-k gate dielectric of 1.0 nm equivalent oxide thickness (EOT) and dual metal gates with different work functionsSourced (the abstract gives no deposition method).
ASM's 2025 annual report says that in advanced transistor structures ALD is concentrated in functional layers such as high-k dielectrics, dipole layers for multi-Vt and work-function metals. It expects these transistor layers to account for about 50% of ALD layers at the 2 nm node and about 60% at the 1.4 nm node (the manufacturer's outlook)Not yet confirmed. It also began shipping its first applications of molybdenum (Mo) ALD at 2 nm, and expects Mo ALD to replace more of the existing metal as dimensions shrink (the manufacturer's outlook)Not yet confirmed. It also states that ALD adoption is growing in MIM capacitors and backside-power architecturesSourced.
(2) The DRAM capacitor
Rhee et al. (2025, peer-reviewed) state that the dielectric of commercial DRAM cell capacitors is ZrO2/Al2O3/ZrO2 (ZAZ), based on tetragonal ZrO2Sourced. Leakage current flows along ZrO2 grain boundaries, and an amorphous Al2O3 layer is inserted to block it, but Al2O3's permittivity (about 9) is lower than ZrO2's (about 40), so the overall k falls. With further scaling, only a few cycles of Al2O3 ALD are therefore used to suppress leakageSourced. The same paper reports that area-selective ALD growing Al2O3 only on ZrO2 grain boundaries raised the overall dielectric constant by 15.5% without increasing leakage (laboratory samples)Sourced.
(3) Spacers
A gate spacer protects the sidewalls of the gate and defines the regions of ion implantation. Meng et al.'s 2016 review lists the requirements on gate spacers: uniform thickness across the wafer (conformal, with a small loading effect), a steep sidewall shape, and a low wet etch rate (to keep the high-k metal gate safe from later cleaning and etching). It introduces examples of PEALD SiNx used as spacer and encapsulation liner in 32/28 nm HKMGSourced. The spacer films of multiple patterning in our explainer on lithography and EUV are films of the same kind.
(4) Barrier layers and electrodes
Baishya et al. state that TiN is used as a diffusion barrier in ultra-large-scale integration (ULSI) and as a capacitor electrode in DRAMSourced. To work as a barrier even when extremely thin, the film needs continuity and purity, and as we saw, ultrathin TiN shows strong effects in resistivity and surface oxidation.
The three examples in this article are all a few nanometres thick or less, and their values are not set by the bulk properties of the material. TiN's resistivity rises about 200 times at 4.7 nm, DRAM's Al2O3 is only a few cycles thick, and Al2O3 grown at low temperature carries more carbon impurity and has lower breakdown strength. The points to watch in design are (1) nucleation (early growth) until the film becomes continuous, (2) the interface with the underlayer (the same viewpoint as the multilayer of the EUV mirror in our explainer on lithography and EUV), (3) impurities and defects, and (4) whether it survives the heat, chemicals and plasma of later steps (this article's commentary). Above all, do not compare a value at one thickness on one underlayer with a value under other conditions.
9. The throughput problem: our calculation
ALD's drawback is that it is slow. Poodt et al. (2012, peer-reviewed) say that the major drawback of ALD is its low deposition rate, which makes it less attractive for applications needing high throughput, and present spatial ALD, in which the half-reactions are separated in space instead of by purge steps, as a route to high deposition rate and high throughput without losing the typical ALD assets (focusing on photovoltaics and flexible electronics)Sourced. Oviroh et al.'s review cites a spatial-ALD example reaching a deposition rate of about 3,600 nm/h, while also noting a possible loss of film qualitySourced.
With TiN's GPC (0.047 nm), the time for 2 nm and 5 nm films for three assumed cycle timesOur calculation.
- Laboratory example (19.5 s per cycle, Baishya et al.): 2 nm (about 43 cycles) takes about 13.8 min and 5 nm (about 106 cycles) about 34.6 min
- Assumed (5 s per cycle): about 3.5 min for 2 nm and about 8.9 min for 5 nm
- Assumed (2 s per cycle): about 1.4 min for 2 nm and about 3.5 min for 5 nm
A guide to the number of chambers: if one chamber processes one wafer at a time and eight chambers must handle 60 wafers per hour, each wafer may occupy a chamber for 8 × 60 min ÷ 60 wafers = 8 min at most. For 2 nm (about 43 cycles), that means a cycle time of about 11 s or lessOur calculation. ASM describes its single-wafer thermal ALD tool Synergis as a high-productivity tool that can be configured with up to four dual chamber modules (eight chambers in all) (the manufacturer's description)Sourced.
Assumptions and limits: 19.5 s per cycle is the total of pulses and purges on a laboratory tool, not a production-tool value. 5 s and 2 s are this article's assumptions, and the real production cycle times could not be confirmed here. Wafer loading, heat-up and chamber cleaning are not included.
Precursor utilization is also a problem. Oviroh et al.'s review says that about 60% of the precursor is wasted in ALD and that the utilization of TMA deposited on wafers was about 50.4% in an experimentSourced (quoted by the review; conditions not checked here). Raising the efficiency of speed, precursor and energy together is a challenge for both tools and materials.
Shortening a cycle means shortening pulses and purges. To saturate even with a short pulse, the precursor must adsorb and saturate quickly and desorb quickly in the purge. A low-vapour-pressure precursor makes line temperature control and securing the supply harder (this article's commentary). Together with the fact that deeper structures need longer exposure (Section 6), precursor design bears directly on time per wafer. Using plasma (PEALD), spatial separation and multiple chambers are solutions from the tool side rather than the material side (commentary).
10. How to read the numbers: keep laboratory, manufacturer's outlook and calculation apart
| Number | What it is | Category | Caution |
|---|---|---|---|
| About 1.1 Å/cycle (150 °C and above), about 0.9 (80 °C) | Growth rate of TMA/water Al2O3 | Peer-reviewed paper (2022, ellipsometry) | A laboratory traveling-wave reactor. 40 s purge |
| About 0.047 nm/cycle; 19.5 s per cycle | Growth rate and cycle time of TiN from TiCl4/NH3 at 400 °C | Peer-reviewed paper (2026) | A laboratory tool. Not a production cycle time |
| About 100,000 / about 540 µΩ·cm | Resistivity of TiN at 4.7 nm / 18.8 nm (sheet resistance × thickness) | Our calculation (the paper's sheet resistance and nominal thickness) | On glass, before exposure. Breakdown not checked |
| Aspect ratio 43 | The hole coated completely uniformly with HfO2 | Peer-reviewed paper (2003) | Laboratory conditions. Not the same as production structures |
| k ≈ 9 / ≈ 40; 15.5% | Permittivity of Al2O3 / ZrO2; the rise in overall permittivity from grain-boundary-selective ALD | Peer-reviewed paper (2025) | 15.5% is for a laboratory sample |
| EOT 1.0 nm | The high-k gate dielectric first used in volume production at 45 nm | Paper abstract (2007) | The abstract gives no deposition method |
| 50% to 60% | Share of transistor layers in ALD layers (2 nm to 1.4 nm) | Manufacturer's outlook (2025) | Not yet confirmed |
| About 3,600 nm/h | An example deposition rate of spatial ALD | Quoted by a review | Not necessarily at the quality level of semiconductor films |
| 13.8, 34.6 min and others | Calculated TiN deposition times | Our calculation | Cycle times other than 19.5 s are assumptions |
11. Limits and what we could not confirm
(1) We could not confirm actual cycle times or growth rates of production tools
The GPC values and cycle time used here are all values from laboratory-tool papers. We found no concrete throughput figures for production ALD tools in the manufacturer's technical material, so we could not confirm them.
(2) We could not confirm how high-k films are deposited in logic
Mistry et al.'s abstract does not state how the high-k gate dielectric was deposited. ASM says its ALD tools (such as Pulsar) are used for high-k metal gates, but whether a particular company's process is ALD could not be confirmed from the primary sources used here.
(3) Precursor safety and regulation are not covered
The safety and environmental regulation of precursors and reactants (pyrophoric organometallics, corrosive halides, toxic gases and so on) is outside the scope of this article. Handling follows the supplier's SDS and the law. Fluorinated gases and regulation are taken up in our explainer on etching.
(4) Atomic layer etching (ALE) and the integration of deposition and etch come in the next article
Combinations of ALD and etching, such as the correction steps of area-selective ALD, will be organized together with atomic layer etching (ALE) in our explainer on etching.
- ALD stacks a film by repeating self-limiting reactions, and thickness is set by cycles × GPCSourced
- Al2O3 (TMA/water) grows at about 1.1 Å per cycle and TiN (TiCl4/NH3) at about 0.047 nm per cycle (both laboratory). 10 nm is about 91 and about 213 cyclesOur calculation
- Plasma ALD offers lower temperature and more freedom in materials, but conformality in deep structures can fall and plasma damage is a concernSourced
- Uniform coverage of deep holes (HfO2 at aspect ratio 43) is ALD's strength, and area-selective ALD keeps its selectivity with correction steps such as selective etchingSourced
- In ultrathin films, continuity, interfaces and impurities set the values. The resistivity of 4.7 nm TiN is about 200 times that of 18.8 nmOur calculation
- The biggest problem is time. Under laboratory conditions a 5 nm TiN film takes about 35 minutes by our calculation, and production cycle times could not be confirmed
12. Glossary
- ALD
- Atomic layer deposition. Film growth by alternating self-limiting reactions.
- Precursor
- The molecule that carries the film's element (a metal, for example). Examples: TMA, TiCl4.
- Reactant (co-reactant)
- The substance that supplies oxygen, nitrogen and so on by reacting with the precursor: water, NH3, plasma.
- Purge
- The step that removes excess molecules and by-products with inert gas.
- GPC
- Growth per cycle. The film thickness added in one cycle.
- ALD window
- The temperature range in which GPC is nearly constant.
- PEALD
- Plasma-enhanced ALD. Uses plasma in the reactant step.
- Conformal
- Coating evenly, following steps and holes, with uniform thickness.
- Aspect ratio (AR)
- Depth ÷ width of a hole or trench.
- Area-selective ALD
- ALD that grows film only on a chosen material (AS-ALD).
- EPE
- Edge placement error. The displacement of a pattern edge.
- High-k
- An insulating material with a higher permittivity than SiO2, such as HfO2.
- EOT
- Equivalent oxide thickness. The thickness of SiO2 that would give the same capacitance.
- GAA
- Gate-all-around. A structure in which the gate surrounds the channel (nanosheet) on all sides.
- Spatial ALD
- ALD that separates the half-reactions in space instead of using purge steps.
13. References (primary sources)
- Puurunen RL "Surface chemistry of atomic layer deposition: A case study for the trimethylaluminum/water process", J. Appl. Phys. 97(12), 121301 (2005, peer-reviewed review) — doi.org/10.1063/1.1940727
- Oviroh PO et al. "New development of atomic layer deposition: processes, methods and applications", Sci. Technol. Adv. Mater. 20(1), 465–496 (2019, peer-reviewed review, open access) — doi.org/10.1080/14686996.2019.1599694
- Kim S et al. "Influence of growth temperature on dielectric strength of Al2O3 thin films prepared via atomic layer deposition at low temperature", Sci. Rep. 12, 5124 (2022, peer-reviewed) — doi.org/10.1038/s41598-022-09054-7
- Meng X et al. "Atomic Layer Deposition of Silicon Nitride Thin Films: A Review of Recent Progress, Challenges, and Outlooks", Materials 9(12), 1007 (2016, peer-reviewed review) — doi.org/10.3390/ma9121007
- Baishya K et al. "Comprehensive study of ultrathin TiN films by ALD: influence of film thickness and substrate on composition, structure, sheet resistance and durability", Nanoscale Adv. 8(8), 2777–2786 (2026, peer-reviewed) — doi.org/10.1039/d5na01134e
- Gordon RG et al. "A Kinetic Model for Step Coverage by Atomic Layer Deposition in Narrow Holes or Trenches", Chem. Vap. Deposition 9(2), 73–78 (2003, peer-reviewed) — doi.org/10.1002/cvde.200390005
- Profijt HB et al. "Plasma-Assisted Atomic Layer Deposition: Basics, Opportunities, and Challenges", J. Vac. Sci. Technol. A 29(5), 050801 (2011, peer-reviewed review) — doi.org/10.1116/1.3609974
- ASM International "ALD (Atomic Layer Deposition)", technology and products page (the manufacturer's description), accessed 9 October 2026 — asm.com
- Mackus AJM et al. "From the Bottom-Up: Toward Area-Selective Atomic Layer Deposition with High Selectivity", Chem. Mater. 31(1), 2–12 (2019, peer-reviewed perspective) — doi.org/10.1021/acs.chemmater.8b03454
- Rhee M-J et al. "Area-Selective Atomic Layer Deposition on Homogeneous Substrate for Next-Generation Electronic Devices", Adv. Sci. 12(22), 2414483 (2025, peer-reviewed, open access) — doi.org/10.1002/advs.202414483
- Mistry K et al. "A 45nm Logic Technology with High-k+Metal Gate Transistors, Strained Silicon, 9 Cu Interconnect Layers, 193nm Dry Patterning, and 100% Pb-free Packaging", IEDM 2007, 247–250 (2007, abstract of the paper) — doi.org/10.1109/IEDM.2007.4418914
- Wilk GD, Wallace RM, Anthony JM "High-κ gate dielectrics: Current status and materials properties considerations", J. Appl. Phys. 89(10), 5243–5275 (2001, peer-reviewed review) — doi.org/10.1063/1.1361065
- ASM International "Annual Report 2025" (the manufacturer's annual report, PDF) — asm.com
- Poodt P et al. "Spatial atomic layer deposition: A route towards further industrialization of atomic layer deposition", J. Vac. Sci. Technol. A 30(1), 010802 (2012, peer-reviewed review) — doi.org/10.1116/1.3670745
14. Claim-to-source audit
| Claim in the text | Basis | Label |
|---|---|---|
| The definition of ALD as a CVD technique based on sequential self-terminating gas–solid reactions, its use for about four decades for conformal inorganic layers down to nanometre thickness, and TMA/water as a "rather ideal ALD process" | Puurunen (2005, abstract of the peer-reviewed review) [Source 1] https://doi.org/10.1063/1.1940727 | Sourced |
| The four steps (precursor, purge, reactant, purge); the difference from CVD (self-limiting adsorption, alternating introduction); the ALD window; thermal ALD at 150 to 350 °C driven by surface reactions with easy conformality; the low-temperature benefit of PEALD; radical recombination in deep structures (an introduction of Knoops et al.'s work); about 3,600 nm/h for spatial ALD with possible loss of film quality; about 60% of precursor wasted and about 50.4% TMA utilization | Oviroh et al. (2019, peer-reviewed review). Numbers are quoted by the review [Source 2] https://doi.org/10.1080/14686996.2019.1599694 | Sourced |
| TMA/water Al2O3: a traveling-wave reactor, 80 to 250 °C, GPC of about 0.9 Å at 80 °C and about 1.1 Å at 150 °C and above (the ALD window), 40 s purge, the slope of thickness versus cycles by spectroscopic ellipsometry, the reason for the drop below 150 °C (activation barrier of CH3 removal), more carbon impurity and oxygen defects at low temperature lowering breakdown strength, and about 8.3 MV/cm for the 150 °C film | Kim et al. (2022, peer-reviewed). Laboratory samples [Source 3] https://doi.org/10.1038/s41598-022-09054-7 | Sourced |
| SiNx ALD: thermal ALD with chlorosilanes plus NH3 (or hydrazine), typically above 450 °C; PEALD typically below 500 °C; examples of 300 to 500 °C PEALD SiNx as spacer and encapsulation liner for 32/28 nm HKMG; and gate-spacer requirements (uniform thickness, sidewall shape, low wet etch rate) | Meng et al. (2016, peer-reviewed review) [Source 4] https://doi.org/10.3390/ma9121007 | Sourced |
| TiN: TiCl4 and NH3 at 400 °C; the cycle breakdown (0.5, 4, 2.5, 5, 2.5 and 5 s); about 0.047 nm/cycle; 4.7 to 18.8 nm for 100 to 400 cycles; sheet resistance (222.3 kΩ/sq, 2.5 kΩ/sq, 519 Ω/sq, 287 Ω/sq); 540 µΩ·cm; XPS oxygen (about 30%, 20%, 21%, 18%) and XPS probing the top 5 to 10 nm; and TiN's use as a diffusion barrier and DRAM electrode | Baishya et al. (2026, peer-reviewed). Laboratory tool, on glass [Source 5] https://doi.org/10.1039/d5na01134e | Sourced |
| That HfO2 from a hafnium amide and water coated holes of aspect ratio 43 completely conformally; the two conditions for uniform coverage (a minimum amount of vapour, and a minimum product of vapour pressure and exposure time at the entrance); and that simple scaling laws were derived | Gordon et al. (2003, abstract of the peer-reviewed paper) [Source 6] https://doi.org/10.1002/cvde.200390005 | Sourced |
| That plasma-assisted ALD widens the choice of material properties, substrate temperature, precursors and conditions, while conformality can fall and plasma damage is a concern | Profijt et al. (2011, abstract of the peer-reviewed review) [Source 7] https://doi.org/10.1116/1.3609974 | Sourced |
| ALD definition, cycle and self-limiting nature; thermal ALD and PEALD (PEALD allows lower temperatures for low-thermal-budget uses); applications (high-k metal gates, spacer dielectrics for patterning, MIM capacitors, gate spacers, high-aspect-ratio gap-fill); that Synergis can be configured with up to four dual chamber modules (eight chambers); and that Pulsar is used for high-k dielectrics | ASM International technical and product page (manufacturer's description) [Source 8] https://www.asm.com/our-technology-products/ald | Sourced |
| Why area-selective ALD is gaining momentum in semiconductors (eliminating edge placement errors), the general cause of lost selectivity, and the idea of correction steps, multistep cycles and supercycles | Mackus et al. (2019, abstract of the peer-reviewed perspective) [Source 9] https://doi.org/10.1021/acs.chemmater.8b03454 | Sourced |
| That the DRAM capacitor dielectric is ZrO2/Al2O3/ZrO2 with k values (Al2O3 about 9, ZrO2 about 40) and only a few cycles of Al2O3 ALD; the area-selective examples (W growing only on H-terminated Si) and that many studies lose selectivity after a certain number of cycles; and that grain-boundary-selective Al2O3 raised the overall dielectric constant by 15.5% without more leakage | Rhee et al. (2025, peer-reviewed, open access). Laboratory samples [Source 10] https://doi.org/10.1002/advs.202414483 | Sourced |
| That the 45 nm logic technology first incorporated high-k + metal-gate transistors in a volume manufacturing process, with 1.0 nm EOT and dual band-edge work-function metal gates (the abstract gives no deposition method) | Mistry et al. (2007, abstract of the paper) [Source 11] https://doi.org/10.1109/IEDM.2007.4418914 | Sourced |
| The guidelines for choosing a gate dielectric to replace SiO2 (permittivity, band gap and band alignment, thermodynamic stability, film morphology, interface quality, process compatibility, reliability) | Wilk et al. (2001, abstract of the peer-reviewed review) [Source 12] https://doi.org/10.1063/1.1361065 | Sourced |
| That the 3D structure of GAA calls for additional ALD steps; that 2025 was the GAA ramp year; that transistor layers (high-k, dipole layers, work-function metals) are expected to be about 50% of ALD layers at 2 nm and about 60% at 1.4 nm; the first Mo ALD shipments at 2 nm; growing ALD adoption in MIM capacitors and backside power; and that XP8E supports selective deposition | ASM International Annual Report 2025 (the manufacturer's statements and outlook) [Source 13] https://www.asm.com/downloads/232221-annual-interim-reports/annual-report-2025 | Sourced |
| That the big drawback of ALD is its low deposition rate, and that spatial ALD is a route to high deposition rates | Poodt et al. (2012, abstract of the peer-reviewed review) [Source 14] https://doi.org/10.1116/1.3670745 | Sourced |
| About 91 and about 213 cycles for 10 nm (divided by 1.1 Å and 0.047 nm); cycles × cycle time (about 43 cycles for 2 nm TiN: 13.8, 3.5, 1.4 min; about 106 cycles for 5 nm: 34.6, 8.9, 3.5 min); under 8 min per wafer for 60 wafers/h on 8 chambers, so about 11 s per cycle or less at 2 nm; and (86÷43)² = about 4 times and (100÷43)² = about 5.4 times | Our calculation. GPC values are laboratory reports. Cycle times other than 19.5 s and the square law are this article's assumptions. Production cycle times could not be confirmed | Our calculation |
| TiN resistivity = sheet resistance × thickness (4.7 nm: about 100,000 µΩ·cm; 9.4 nm: about 2,350; 14.1 nm: about 730; 18.8 nm: about 540; the 4.7 nm film being about 200 times the 18.8 nm film) | Our calculation. Sheet resistance is from the paper (on glass, before exposure); thickness is the nominal value from the growth rate. The breakdown of the increase was not checked | Our calculation |
| That insufficient purge mixes in CVD-like growth; the four conditions on precursors; thermal budget as the reason for PEALD's lower temperature; the three demands of low temperature, deep structures and low damage; selective ALD as a combination of deposition and etch; the framing that continuity, interface and impurities set the values in ultrathin films; the framing that precursor saturation speed and vapour pressure affect throughput; and each materials-engineer box | This article's organization and commentary based on the published content. Specifications of individual materials were not confirmed | Commentary |
| Actual cycle times and throughput of production ALD tools, whether a particular company's high-k deposition is necessarily ALD, and precursor safety and regulation | Could not be confirmed from primary sources within the scope of this article, so not stated | Commentary |
| That Figs. 2, 3 and 5 to 8 are explanatory drawings, not real design or measurement drawings, and that Figs. 1 and 4 are AI-generated images | This article's note | Commentary |
Last updated: 9 October 2026 / Sources are limited to primary material (peer-reviewed papers, the manufacturer's official pages and annual report). Because structural readings and materials-design interpretations are included, they are marked as "Commentary" and kept apart from sourced facts. Actual cycle times and throughput of production ALD tools, the deposition method of any particular company's high-k layer, and precursor safety and regulation could not be confirmed, so they are not stated. Growth rates and resistivities are laboratory reports, not production values. Company figures and outlooks are the companies' own statements. The figures are explanatory diagrams. Figs. 2, 3 and 5 to 8 are vector drawings and Figs. 1 and 4 are AI-generated images; none of them shows an actual photograph or design of a tool, film or structure.