TECHNOLOGY EXPLAINER
Additive Manufacturing for Space
— Rocket-engine parts, satellite parts and printing in orbit: how far has it come?
Additive manufacturing (3D printing) builds complex shapes in one piece by melting and stacking material layer by layer. In space it has been used on rocket-engine combustion chambers and injectors, among others, to cut part count, schedule and cost. Written for materials engineers who know little about space engineering, this article uses diagrams to explain the differences between processes, real NASA engine parts, how surface roughness and powder variation turn into performance, alloys developed for printing, and the problem of quality assurance and qualification (the layers of standards). Finally it separates, as far as could be confirmed, what has actually been done in orbital additive manufacturing from what was planned or ended.
- The short version / what to know first / where this fits
- What additive manufacturing is: three representative processes
- Rocket-engine parts: NASA examples
- Surface roughness becomes performance
- Alloys made for printing
- Variation and failure: why quality assurance is hard
- Additive manufacturing for satellite parts
- The qualification framework: layers of standards
- Additive manufacturing in orbit: the extent of demonstrations
- How to read the yardsticks and standards / glossary / references / claim-to-source audit
Sourced = stated in a published source (linked)
Our calculation = a value this article calculated from stated assumptions
Not yet confirmed = company targets, plans, drafts of standards, and other items not yet settled
Our own reading for materials engineers is marked as commentary. Inference is shown in bold. Every analogy comes with a note on where it stops working.
Cost, part count, test time and alloy performance are statements in NASA reports and are conditional values. "Expected to cut cost by a factor of four" is an expectation, not an achieved value for flight hardware. Alloy multipliers (such as GRX-810) depend on the conventional alloy compared and its conditions. Fig. 4 shows relative values we plotted from NASA statements. For orbital manufacturing, what was done is separated from what was planned or ended. Failures are described neutrally within published presentations and causes are not asserted by inference. Check date: 17 October 2026. Military applications are not covered.
1. The short version, what to know first, and where this fits
- Additive manufacturing makes not only the shape but the inside of the material. Because material is melted and solidified, microstructure, pores, surface roughness and residual stress are set by build conditions and powder. A NASA study of Alloy 718 reported variation in composition, fines, morphology and size distribution across 16 commercial powders.Sourced[Ref. 8]
- For engine parts, experience has accumulated. NASA Marshall has used metal additive manufacturing since 2010 and built combustion hardware from the 100 lbf to 35,000 lbf class, hot-fire testing many parts.Sourced[Ref. 1] Yet a 2022 NASA presentation reports a powder-bed-fusion copper-alloy combustion chamber that failed during a hot-fire test due to degraded material quality from an additive-manufacturing process issue.Sourced[Ref. 7]
- Metal printing in orbit is still short of demonstration. What has run on the ISS is mainly polymer printing; metal machines stayed at the development stage and related projects ended or were cancelled in 2023.Sourced[Refs. 17, 19, 20, 21]
No space knowledge is needed. It is enough to imagine that melting and solidifying metal gives structure and defects similar to casting or welding. Reading our explainer on rocket engines and propellants (combustion chamber, regenerative cooling) first helps.
Rocket engines and propellants covers copper-alloy chambers and GRCop alloys, lightweight structural materials covers metal weight reduction, and reading space-materials evaluations covers the idea of qualification. This article covers how those materials are made and how they are assured.
2. What additive manufacturing is: three representative processes
Additive manufacturing is a general term for building shape by adding material bit by bit. Terminology is set by ISO/ASTM 52900 (fundamentals and vocabulary).Sourced[Ref. 26] For metals, NASA Marshall has used powder bed fusion (spreading a thin powder layer and melting it with a laser; also called SLM) most often, and has also used laser directed energy deposition, arc deposition and laser-wire deposition.Sourced[Ref. 1]
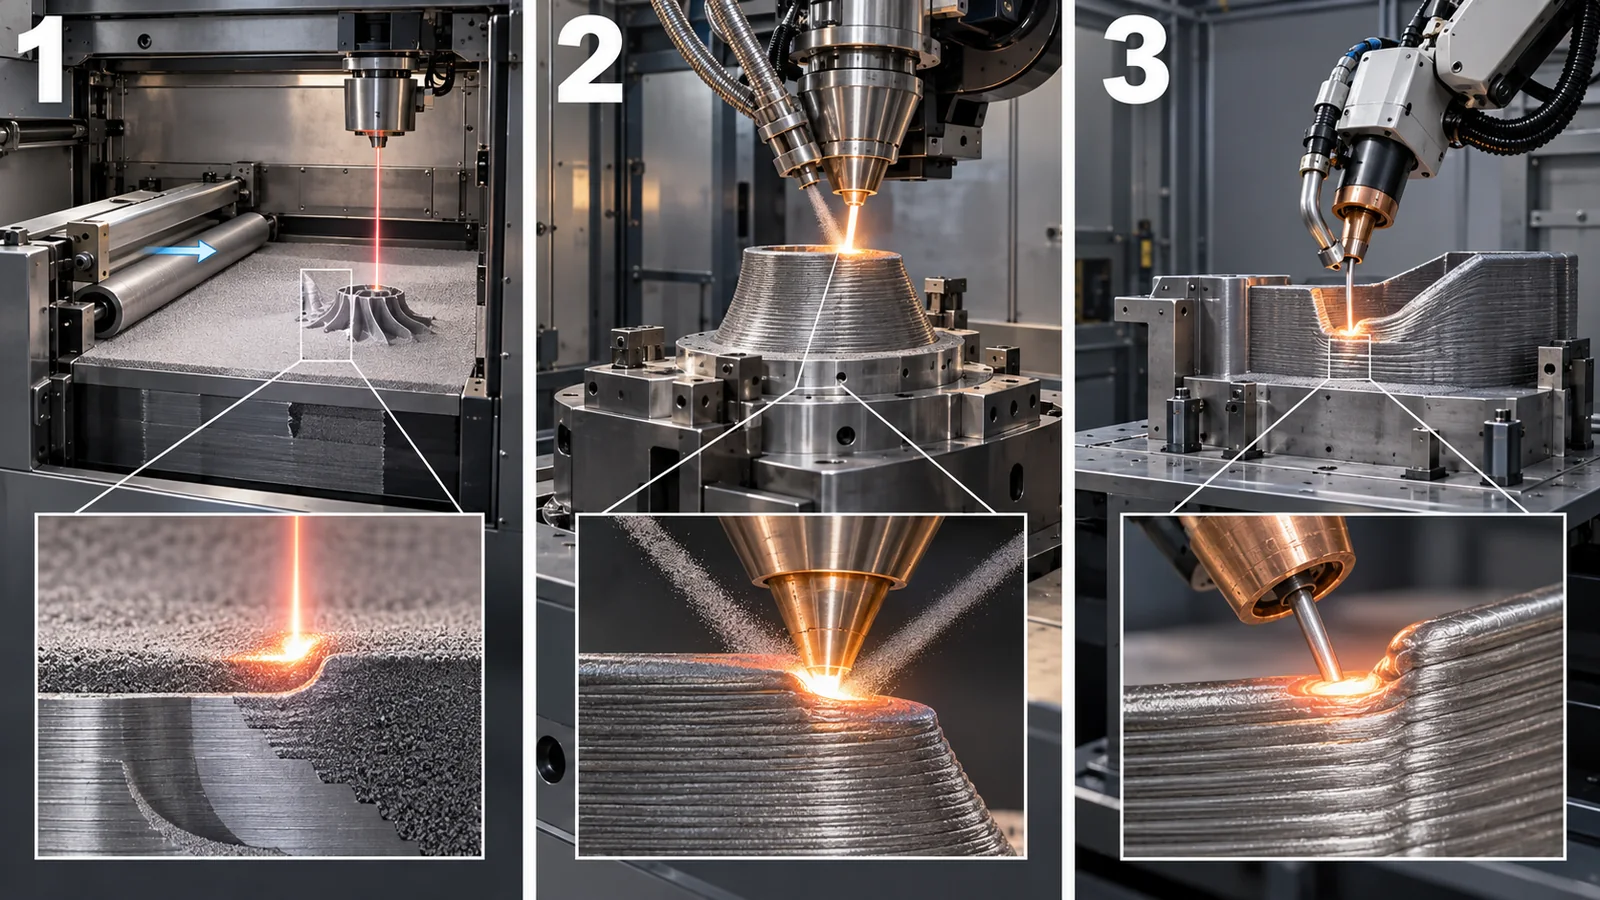
View original SVG, values and sources
Original SVG reference: Conceptual diagram (vector drawing). Schematic of three representative metal additive-manufacturing processes. Descriptions follow NASA Marshall reports.
NASA summarizes the advantages as lower cost, shorter schedules, higher reliability from fewer joints, and better performance from designs not feasible by conventional means, by replacing complicated and expensive metal parts.Sourced[Ref. 1] Printing in one piece removes brazed or welded joints, which is the main aim for engine parts.
3. Rocket-engine parts: NASA examples
NASA Marshall has used metal additive manufacturing for liquid rocket engine parts since 2010. It has designed and built combustion hardware from the 100 lbf to 35,000 lbf class (injectors, regeneratively cooled chambers and nozzles, gas-generator and preburner parts, and igniters) by powder bed fusion and deposition processes, and hot-fire tested many.Sourced[Ref. 1] L3Harris also says that its next-generation RS-25 engines will include advanced manufacturing techniques including 3D printingSourced[Ref. 13] (company statement).
Conventionally an injector is made of many parts, each made and inspected, then joined by brazing, bonding or welding. NASA says additive manufacturing is especially attractive for cutting injector cost because it avoids handling and assembling those piece parts.Sourced[Ref. 1] A 2016 NASA presentation reports that an augmented spark igniter for the RS-25 was printed with an expected cost cut of about a factor of four, that part count fell by 45% in a liquid-hydrogen turbopump, and that a test engine built from printed parts was tested seven times in 2016.Sourced[Ref. 2]
Printing copper-alloy chambers was an especially hard challenge. NASA says copper alloys are highly reflective and conductive, making it hard to melt the powder with a laser. NASA Marshall and Glenn developed powder-bed-fusion processes for GRCop (copper-chromium-niobium) alloys from 2014 and showed through characterization and hot-fire tests that GRCop-84 and GRCop-42 are suitable for combustion chambers. Bimetallic chambers combining GRCop-84 liners with superalloy jackets were also built by directed energy deposition.Sourced[Ref. 3] GRCop-42 is reported to reach strength equal to wrought material and conductivity above GRCop-84Sourced[Ref. 4] (alloys are covered in our rocket-engines explainer).
4. Surface roughness becomes performance
An as-built surface is rough. A NASA paper describes the effects in two examples. First, in an injector, only the oxygen bores were honed because the rough surface harms swirl momentum; the only machining needed after removal from the build plate was threads for the igniter and this honing.Sourced[Ref. 1]
Second, a GRCop-84 chamber liner. The first liner showed no erosion of the hot wall after 2,365 s and 25 starts, but its pressure drop was higher than predicted because of the surface roughness of the cooling channels. A second liner of the same configuration, built by a commercial vendor, had about 50% lower roughness and over 20% lower coolant pressure drop in water-cooling tests.Sourced[Ref. 1]
Metal surface roughness not only starts fatigue cracks but changes coolant flow and cooling performance. Internal passages are often out of reach of polishing tools, so the as-built surface remains. For materials engineers, the distribution of surface roughness must be managed as a design input, like a material property (our commentary).
5. Alloys made for printing
In additive manufacturing, besides printing existing alloys, alloys designed around the printing process are being developed. NASA reports three examples.
NASA HR-1 is a high-strength iron-nickel superalloy designed to resist high-pressure hydrogen, hydrogen embrittlement, oxidation and corrosion. NASA says it has good hydrogen resistance, high conductivity, low-cycle-fatigue performance, and high elongation and strength, meeting the requirements of liquid rocket engine parts. Subscale and full-scale channel-wall nozzles have been built by directed energy deposition and hot-fire tested.Sourced[Ref. 5] GRX-810 is a nickel-cobalt-chromium oxide-dispersion-strengthened alloy designed with integrated computational materials engineering (ICME), with nano-scale yttria particles dispersed throughout. NASA says that against conventional nickel superalloys it has twice the tensile strength, 1,000 times better creep and twice the oxidation resistanceSourced[Ref. 6] (NASA statement).
Conventional alloys have compositions set for casting and forging, so in additive manufacturing, with its rapid melting and solidification, cracks and pores can appear. HR-1 and GRX-810 are alloys whose composition and structure were designed from both the printing process and the service environment (high-pressure hydrogen, high temperature). For materials engineers, designing process and alloy together is the real meaning of additive manufacturing (our commentary). Flight heritage for these alloys could not be confirmed here.
6. Variation and failure: why quality assurance is hard
Quality in additive manufacturing is hard because the sources of variation are linked from powder to finished part.
NASA Langley describes quality variation in powder bed fusion as variation by location within a build. Where geometry differs, as in a thin wall versus a bulk, the chosen laser parameters may stop being acceptable and lack-of-fusion or keyhole (deep-penetration) porosity can form. It adds that if parameters drift during a build, it is hard to judge whether the part will still perform.Sourced[Ref. 9]
A failure case: a powder-bed-fusion copper-alloy combustion chamber
A 2022 NASA Marshall presentation reports a powder-bed-fusion copper-alloy combustion chamber that failed during a hot-fire test. The test was meant to show a high duty cycle within a risk-tolerant development project designed so that component failure would have little consequence. According to the presentation, the cause was degraded material quality from an additive-manufacturing process issue. The investigation evaluated the failed chamber, other chambers built at the same time, and representative samples with intentional build witness lines, and summarizes results and recommendations. The presentation says the case showed the need for robust material characterization and rigorous process control and in part motivates the certification approach NASA adopted in NASA-STD-6030.Sourced[Ref. 7]
NASA discloses failure cases as failures within risk-tolerant projects and reflects the lessons in revisions of its standard (NASA-STD-6030). A 2026 NASA presentation likewise says lessons learned from applying the standard (tailoring of requirements, documentation, conservative approaches to developing mechanical properties) will influence future revisions.Sourced[Ref. 11] A culture of sharing failure information advances the discussion of material quality. The detailed cause of the failure is not given within the published abstract, and this article does not speculate.
7. Additive manufacturing for satellite parts
Satellites rarely see the temperatures and pressures of a rocket engine, so additive manufacturing is valued for freedom of shape and short lead time. Three NASA examples at different stages follow.
| Example | What it is (source) | Stage |
|---|---|---|
| GPX2 3U CubeSat bus | NASA Langley made the bus a one-piece structure of Windform XT 2.0 (a polymer composite) by laser sintering instead of milling metal. It included features unrealizable by milling, with a lead time of about two weeks; milling would have needed several parts per wall with more joints, fasteners and mass.Sourced[Ref. 14] | Developed and launched (NASA report) |
| MoonBEAM 6U CubeSat | A concept study using printed tanks as part of the spacecraft structure, with a denser green propellant.Sourced[Ref. 15] | Mission concept study |
| A printed CubeSat propulsion system | Embedding electronics and wiring in printed structures and taking a commercial pulsed plasma thruster into the printing process; tests of the dielectric strength of the printed material and a proof-of-concept of the printed thruster.Sourced[Ref. 16] | Proof-of-concept |
The GPX2 example is a polymer composite (Windform XT 2.0), not metal additive manufacturing. Flight heritage of metal additively manufactured satellite parts was not found in the primary sources this article could confirm.
8. The qualification framework: layers of standards
The quality of additive manufacturing cannot be assured by inspecting parts alone. The process, machine, operator, powder and post-processing are controlled, and then the part is qualified. Standards form layers from vocabulary through spaceflight requirements to process control for each build method.
NASA-STD-6030 is a NASA technical standard issued as a baseline on 21 April 2021, directed at the design, fabrication and testing of additively manufactured spaceflight hardware (crewed, uncrewed, robotic, launch vehicle, lander and others). It applies in full to crewed spaceflight hardware, has tailoring guidance for uncrewed missions, and intends to cover in-space additive manufacturing too, with significant tailoring expected.Sourced[Ref. 22] MSFC-STD-3716 is a framework for introducing laser powder bed fusion parts into high-reliability spaceflight applications, and MSFC-SPEC-3717 sets procedures for controlling and qualifying the process and equipment and for training personnel (both 18 October 2017).Sourced[Refs. 23, 24] ECSS-Q-ST-70-80C (30 July 2021) gives requirements for processing and quality assurance of metallic powder bed fusion and states that it does not prescribe process parameters and that its principles can serve as a reference for other processes.Sourced[Ref. 25]
As challenges, NASA said in 2023 that a probabilistic damage tolerance assessment (PDTA) is among the most critical needs, including development of computational models, understanding the "effect of defects" and introducing in-situ monitoring and inspection.Sourced[Ref. 10] In other words, a way to show probabilistically which defect sizes and locations are acceptable remains an open challenge.Not yet confirmed
A standard is a framework of processes and documents to follow, not an automatic guarantee of part safety. NASA itself says lessons from applying its standard will be reflected in future revisions.Sourced[Ref. 11] ECSS-Q-ST-70-80C does not set process parameters.Sourced[Ref. 25] Under which conditions a part was built and by which tests it was checked must be confirmed for each part and process.
9. Additive manufacturing in orbit: the extent of demonstrations
The idea of making parts in space is attractive, but what has been done is limited. According to NASA documents, the first Made in Space 3D printer was launched to the ISS in 2014 and showed that an on-demand manufacturing system can run in microgravity. Properties of material made in the second-generation Additive Manufacturing Facility (AMF) were also characterized.Sourced[Ref. 17] These are polymer printers, and replacing ISS polymer parts without waiting for resupply was considered.Sourced[Ref. 18]
For metals, a 2021 NASA report said two ISS demonstration payloads were in development: wire plus arc (Made in Space's Vulcan) and bound metal deposition (Techshot's Fabrication Laboratory).Sourced[Ref. 19] However, NASA's On Demand Manufacturing of Metals (ODMM) project was cancelled in May 2023 and a technology maturation plan was drafted.Sourced[Ref. 20] OSAM-2 (Archinaut One), which would have demonstrated printing structures in orbit, also concluded in 2023 before a flight demonstration.Sourced[Ref. 21] In 2026 a white paper to augment NASA-STD-6030 for off-world manufacturing is at the pre-release stage.Sourced[Ref. 12]
Making metal in orbit requires maturing powder handling (microgravity, safety), melt-pool behavior, heat removal and post-build quality checks separately from the ground. NASA says manufacturing systems for in-space use need a maturation path independent from processes targeted for terrestrial use.Sourced[Ref. 20] NASA-STD-6030 also says in-space printing needs significant tailoring.Sourced[Ref. 22] A process qualified on the ground cannot simply be taken to orbit (our commentary).
10. How to read the yardsticks and standards
The performance of a printed part is set by strength, toughness and fatigue of the material, and also by dependence on orientation and location, defect size and distribution, surface roughness and control of process, machine and operator. A value from one specimen does not guarantee the value in an actual part.
| What is assessed | Typical test or method (name, source) | Standards and guidance (NASA, ECSS, ISO, etc.) | Reading notes |
|---|---|---|---|
| Vocabulary and basics | — | ISO/ASTM 52900:2021 (Published, confirmed).Sourced[Ref. 26] | A joint ISO and ASTM standard. Number, title and status were checked on the ISO page; the ASTM website was not opened. |
| Material properties (orientation and location) | Evaluation and reporting of mechanical properties by build orientation and location | ISO/ASTM 52909:2024 (orientation and location dependence of mechanical properties of metal parts).Sourced[Ref. 28] | Values change with how specimens are taken. Typical values differ from design allowables. |
| Process control, machines, operators, sites | Definition and qualification of the process, calibration and qualification of equipment, and training of personnel.Sourced[Ref. 24] | MSFC-SPEC-3717 (18 October 2017), ISO/ASTM 52941 (aerospace L-PBF machines; 2026 edition), 52942:2020 (operators), 52920:2023 (production sites) and 52904:2024 (PBF for critical applications).Sourced[Refs. 24, 29, 30, 31, 27] | Even a qualified process needs re-qualification when conditions change (general remark). |
| Overall spaceflight requirements | Requirements for design, fabrication and testing of parts, and quality-assurance requirements that do not set process parameters.Sourced[Refs. 22, 25] | NASA-STD-6030 (baseline, 21 April 2021; Active), MSFC-STD-3716 (18 October 2017), ECSS-Q-ST-70-80C (30 July 2021) and NASA-STD-6016.Sourced[Refs. 22, 23, 25, 32] | NASA standards; application to commercial vehicles depends on contracts (could not be confirmed). The requirements were not checked here. |
| Fracture control | Analysis and tests that a part survives cracks and defects | NASA-STD-5019 (Version A with Change 4, change dated 12 July 2024; Active).Sourced[Ref. 33] | Application to defects specific to printed parts was not checked here. |
| Assessing the effect of defects | Computational models, in-situ monitoring and inspection, and probabilistic damage tolerance assessment (PDTA).Sourced[Refs. 10, 9] | Could not be confirmed (standardizing PDTA is described as a challenge).Not yet confirmed | A standard method linking defects to performance is still being established. |
| Confirmation by hot-fire testing | Burning the part for real (accumulated time, number of starts, signs of erosion).Sourced[Ref. 1] | Could not be confirmed (a common standard setting pass or fail for hot-fire tests was not checked). | One pass does not guarantee a pass for another lot or condition. A failure case also exists (2022).Sourced[Ref. 7] |
| ASTM standards | The joint ISO/ASTM standards above. | ASTM standards other than the joint ISO/ASTM ones were not checked (the ASTM website was not opened). | — |
The arrangement of the table is Our calculation (organizing). Numbers, titles and status were checked on the official pages of ISO, the NASA Technical Standards System and ECSS (17 October 2026). Standard texts were not read; only titles and scope are given.
Reading notes (for materials engineers)
- Ground tests and flight differ. Accumulated hot-fire time is a record for a specific part under specific conditions. Experience with printed parts does not carry over when lot or process changes.
- NASA statements differ from independent verification. Alloy multipliers (GRX-810 and others) and cost expectations are NASA statements, and independent verification could not be confirmed.
- Check whether a standard is a recommendation or a requirement. NASA-STD-6030 sets requirements for NASA spaceflight hardware, while ISO/ASTM standards are used when a contract or application standard calls for them.
- Plans and achievements differ. Metal printing in orbit, as far as could be confirmed, is at the stage of plans, endings and cancellations, not achievements.
11. Glossary
- Additive manufacturing (AM)
- Building shape by adding material bit by bit; also called 3D printing.
- Powder bed fusion (L-PBF / SLM)
- Spreading a thin powder layer and melting it with a laser.
- Directed energy deposition (DED)
- Melting powder or wire as it is fed, depositing as you go.
- LWDC
- Laser Wire Direct Closeout: closing cooling channels with wire.
- Build plate
- The metal plate on which the part is built.
- GRCop
- NASA's copper-chromium-niobium alloys.
- NASA HR-1
- A hydrogen-resistant iron-nickel superalloy.
- GRX-810
- NASA's oxide-dispersion-strengthened nickel-cobalt-chromium alloy.
- ODS (oxide dispersion strengthened)
- Dispersing fine oxide particles to raise high-temperature strength.
- ICME
- Integrated computational materials engineering: designing materials and processes by computation.
- Injector
- The part that injects fuel and oxidizer into the chamber.
- Honing
- Finishing the inside of a bore by polishing.
- Lack of fusion / keyhole
- Pores from unmelted gaps / from over-deep melting.
- Build witness line
- A line left at a build seam.
- PDTA
- Probabilistic damage tolerance assessment.
- ISS
- International Space Station.
- AMF
- Additive Manufacturing Facility: the second-generation polymer printer on the ISS.
- OSAM-2 / Archinaut One
- A demonstration plan to print and assemble beams in orbit (concluded in 2023).
- ODMM
- On Demand Manufacturing of Metals, NASA's project (cancelled May 2023).
- NASA-STD-6030
- NASA's additive-manufacturing requirements for spaceflight.
- ISO/ASTM
- The designation of joint ISO and ASTM standards.
- ECSS
- European Cooperation for Space Standardization.
- CubeSat
- A small satellite built in units of 10 cm cubes.
12. References
- Gradl P. et al. (NASA Marshall) "Additive Manufacturing of Liquid Rocket Engine Combustion Devices: A Summary of Process Developments and Hot-Fire Testing Results", AIAA-2018-4625 — ntrs.nasa.gov/citations/20180006344
- West B. et al. (NASA Marshall) "Additive Manufacturing for Affordable Rocket Engines" (2016) — ntrs.nasa.gov/citations/20160012051
- Gradl P. R. et al. (NASA Marshall) "Progress in Additively Manufactured Copper-Alloy GRCop-84, GRCop-42, and Bimetallic Combustion Chambers for Liquid Rocket Engines" (2019) — ntrs.nasa.gov/citations/20190033311
- Gradl P. R. et al. (NASA Marshall) "GRCop-42 Development and Hot-fire Testing Using Additive Manufacturing Powder Bed Fusion for Channel-Cooled Combustion Chambers" (2019) — ntrs.nasa.gov/citations/20190030433
- Gradl P. R. et al. (NASA Marshall) "Integral Channel Nozzles and Heat Exchangers using Additive Manufacturing Directed Energy Deposition NASA HR-1 Alloy" (2022) — ntrs.nasa.gov/citations/20220013530
- Gradl P. R. et al. (NASA) "Extreme Temperature Additively Manufactured GRX-810 Alloy Development and Hot-fire Testing for Liquid Rocket Engines" (2024) — ntrs.nasa.gov/citations/20230017675
- Gradl P. et al. (NASA Marshall) "Having a Come-Apart: Lessons Learned from Additively Manufactured Hardware Failures" (2022) (the abstract of the presentation was checked) — ntrs.nasa.gov/citations/20220016137
- Smith T. M. et al. (NASA Glenn) "Relationship of Powder Feedstock Variability to Microstructure and Defects in Selective Laser Melted Alloy 718" (2017) (the abstract of the talk was checked) — ntrs.nasa.gov/citations/20170008114
- Richter B. et al. (NASA Langley) "Towards Integrated Computational Materials Engineering for Quantifying Performance Impacts of Microstructure and Defect Interactions in Powder Bed Fusion Parts" (2023) (the abstract of the talk was checked) — ntrs.nasa.gov/citations/20230014203
- Tilson W. et al. (NASA) "NASA's Certification and Qualification Challenges for Additively Manufactured Hardware: What Is Next?" (2023) — ntrs.nasa.gov/citations/20230003172
- Poe T., Juarez T. (NASA) "A Frank Discussion on Lessons Learned From Adopting and Applying NASA-STD-6030 for Spaceflight Systems" (2026) (the abstract of the presentation was checked) — ntrs.nasa.gov/citations/20260004731
- Chytka M. et al. (NASA) "Off-World Additive Manufacturing - Augmenting NASA-STD-6030" (2026) (the abstract of the slides was checked; the white paper was not yet released) — ntrs.nasa.gov/citations/20260004879
- L3Harris "RS-25 engine" (company statement; checked 17 October 2026) — l3harris.com/all-capabilities/rs-25-engine
- Stark A. et al. (NASA Langley) "Windform XT 2.0 Use as 3U CubeSat Primary Structure" (2023) — ntrs.nasa.gov/citations/20230008181
- Hopkins R. C. et al. (NASA Marshall) "Additive Manufacturing: An Enabling Technology for the MoonBEAM 6U CubeSat Missions" (2017) (a mission concept study) — ntrs.nasa.gov/citations/20170010146
- Marshall W. M. et al. (NASA Glenn) "Using Additive Manufacturing to Print a CubeSat Propulsion System" (2015) (proof-of-concept; the abstract was checked) — ntrs.nasa.gov/citations/20150021276
- Prater T. et al. (NASA Marshall) "NASA's In-Space Manufacturing Project: Update on Manufacturing Technologies and Materials to Enable More Sustainable and Safer Exploration" (2019) — ntrs.nasa.gov/citations/20190033333
- Muhlbauer R. et al. (NASA Marshall) "Building a Plastics Fabrication Laboratory on the ISS: FabLab, MANTIS, Refabricator, CRISSP, ERASMUS, and MAMBA" (2018) (only the abstract was checked) — ntrs.nasa.gov/citations/20180006339
- Prater T. et al. (NASA Marshall) "Adaptation of Metal Additive Manufacturing Processes for the International Space Station" (2021) — ntrs.nasa.gov/citations/20205011519
- Roberts C. E. et al. (NASA Marshall) "NASA Technology Maturation Plan for In-space Manufacturing of Metals" (2023) — ntrs.nasa.gov/citations/20230012701
- NASA "On-Orbit Servicing, Assembly, and Manufacturing 2 (OSAM-2)" (mission page) (checked 17 October 2026) — www.nasa.gov/mission/on-orbit-servicing-assembly-and-manufacturing-2-osam-2/
- NASA NASA-STD-6030 "Additive Manufacturing Requirements for Spaceflight Systems" (baseline, 21 April 2021) (Active; checked 17 October 2026) — standards.nasa.gov/standard/NASA/NASA-STD-6030
- NASA Marshall MSFC-STD-3716 "Standard for Additively Manufactured Spaceflight Hardware by Laser Powder Bed Fusion in Metals" (18 October 2017) (Active; checked 17 October 2026) — standards.nasa.gov/standard/MSFC/MSFC-STD-3716
- NASA Marshall MSFC-SPEC-3717 "Specification for Control and Qualification of Laser Powder Bed Fusion Metallurgical Processes" (18 October 2017) (Active; checked 17 October 2026) — standards.nasa.gov/standard/MSFC/MSFC-SPEC-3717
- ECSS ECSS-Q-ST-70-80C "Processing and quality assurance requirements for metallic powder bed fusion technologies for space applications" (30 July 2021) (checked 17 October 2026) — ecss.nl/standard/ecss-q-st-70-80c-processing-and-quality-assurance-requirements-for-metallic-powder-bed-fusion-technologies-for-space-applications-30-july-2021/
- ISO/ASTM ISO/ASTM 52900:2021 "Additive manufacturing — General principles — Fundamentals and vocabulary" (Published, confirmed; checked on the ISO page, 17 October 2026) — www.iso.org/standard/74514.html
- ISO/ASTM ISO/ASTM 52904:2024 "Additive manufacturing of metals — Process characteristics and performance — Metal powder bed fusion process to meet critical applications" (Published; checked 17 October 2026) — www.iso.org/standard/82919.html
- ISO/ASTM ISO/ASTM 52909:2024 "Additive manufacturing of metals — Finished part properties — Orientation and location dependence of mechanical properties for metal parts" (Published; checked 17 October 2026) — www.iso.org/standard/87956.html
- ISO/ASTM ISO/ASTM 52941:2026 "Additive manufacturing for aerospace — System performance and reliability tests for laser metal powder-bed fusion machines for metallic materials" (the ISO page gives a publication date of 2026-08; checked 17 October 2026) — www.iso.org/standard/86784.html
- ISO/ASTM ISO/ASTM 52942:2020 "Additive manufacturing — Qualification principles — Qualifying machine operators of laser metal powder bed fusion machines and equipment used in aerospace applications" (Published, confirmed; checked 17 October 2026) — www.iso.org/standard/74949.html
- ISO/ASTM ISO/ASTM 52920:2023 "Additive manufacturing — Qualification principles — Requirements for industrial additive manufacturing processes and production sites" (Published; checked 17 October 2026) — www.iso.org/standard/76911.html
- NASA NASA-STD-6016 "Standard Materials and Processes Requirements for Spacecraft" (Version C with Change 1, change date 15 November 2023) (Active; checked 17 October 2026) — standards.nasa.gov/standard/NASA/NASA-STD-6016
- NASA NASA-STD-5019 "Fracture Control Requirements for Spaceflight Hardware" (Version A with Change 4, change date 12 July 2024) (Active; checked 17 October 2026) — standards.nasa.gov/standard/NASA/NASA-STD-5019
13. Claim-to-source audit
| Claim in the text | Basis | Type |
|---|---|---|
| NASA Marshall additive manufacturing (since 2010, powder bed fusion most used, 100 to 35,000 lbf class, injector machining, GRCop-84 liner test results and pressure drop, about 50% lower roughness and over 20% lower pressure drop, LWDC, summary of advantages) | NASA (Gradl et al., AIAA-2018-4625) Reference 1 https://ntrs.nasa.gov/citations/20180006344 | Sourced |
| Expected igniter cost cut by a factor of four, 45% lower part count of a liquid-hydrogen turbopump, and seven tests of a test engine with printed parts (2016) | NASA (West et al., 2016) Reference 2 https://ntrs.nasa.gov/citations/20160012051 | Sourced |
| The difficulty of printing copper alloys (reflectivity and conductivity), GRCop powder-bed-fusion development (from 2014) and bimetallic chambers | NASA (Gradl et al., 2019) Reference 3 https://ntrs.nasa.gov/citations/20190033311 | Sourced |
| GRCop-42 printed strength equal to wrought and conductivity above GRCop-84 | NASA (Gradl et al., 2019) Reference 4 https://ntrs.nasa.gov/citations/20190030433 | Sourced |
| NASA HR-1 (iron-nickel superalloy, hydrogen resistance, LP-DED, channel-wall nozzles) | NASA (Gradl et al., 2022) Reference 5 https://ntrs.nasa.gov/citations/20220013530 | Sourced |
| GRX-810 (ODS alloy, ICME, twice the tensile strength, 1,000 times the creep and twice the oxidation resistance) | NASA (Gradl et al., 2024) Reference 6 https://ntrs.nasa.gov/citations/20230017675 | Sourced |
| The hot-fire failure of a powder-bed-fusion copper-alloy chamber, the degraded material quality from a process issue, the evaluation and recommendations, and the motivation for NASA-STD-6030 | NASA (Gradl et al., 2022 presentation) Reference 7 https://ntrs.nasa.gov/citations/20220016137 | Sourced |
| Variation among 16 Alloy 718 powders, and quality variation by location in a build (lack of fusion, keyhole) | NASA (Smith et al., 2017; Richter et al., 2023) Reference 8 https://ntrs.nasa.gov/citations/20170008114 Reference 9 https://ntrs.nasa.gov/citations/20230014203 | Sourced |
| PDTA as one of the most critical needs (2023) and lessons from applying the standard influencing future revisions (2026) | NASA (Tilson et al., Poe and Juarez) Reference 10 https://ntrs.nasa.gov/citations/20230003172 Reference 11 https://ntrs.nasa.gov/citations/20260004731 | Sourced |
| Advanced manufacturing including 3D printing for next-generation RS-25 engines | L3Harris official page (company statement) Reference 13 https://l3harris.com/all-capabilities/rs-25-engine | Sourced |
| The Windform XT 2.0 bus of the GPX2 3U CubeSat, the MoonBEAM printed-tank concept and the proof-of-concept of a printed CubeSat propulsion system | NASA (Stark et al., Hopkins et al., Marshall et al.) Reference 14 https://ntrs.nasa.gov/citations/20230008181 Reference 15 https://ntrs.nasa.gov/citations/20170010146 Reference 16 https://ntrs.nasa.gov/citations/20150021276 | Sourced |
| The first ISS 3D printer in 2014, AMF, consideration of replacing polymer parts, metal payloads (Vulcan and Fabrication Laboratory), cancellation of ODMM (May 2023), conclusion of OSAM-2 (2023), and the off-world manufacturing white paper | NASA (Prater et al., Muhlbauer et al., Roberts et al., OSAM-2 page, Chytka et al.) Reference 17 https://ntrs.nasa.gov/citations/20190033333 Reference 18 https://ntrs.nasa.gov/citations/20180006339 Reference 19 https://ntrs.nasa.gov/citations/20205011519 Reference 20 https://ntrs.nasa.gov/citations/20230012701 Reference 21 https://www.nasa.gov/mission/on-orbit-servicing-assembly-and-manufacturing-2-osam-2/ Reference 12 https://ntrs.nasa.gov/citations/20260004879 | Sourced |
| NASA-STD-6030 (21 April 2021, full application to crewed, tailoring for uncrewed, significant tailoring in orbit), MSFC-STD-3716, MSFC-SPEC-3717 (18 October 2017), and numbers, titles, versions and status of NASA-STD-6016 and NASA-STD-5019 | NASA Technical Standards System Reference 22 https://standards.nasa.gov/standard/NASA/NASA-STD-6030 Reference 23 https://standards.nasa.gov/standard/MSFC/MSFC-STD-3716 Reference 24 https://standards.nasa.gov/standard/MSFC/MSFC-SPEC-3717 Reference 32 https://standards.nasa.gov/standard/NASA/NASA-STD-6016 Reference 33 https://standards.nasa.gov/standard/NASA/NASA-STD-5019 | Sourced |
| Number, title and scope of ECSS-Q-ST-70-80C (30 July 2021; does not prescribe process parameters) | ECSS official page Reference 25 https://ecss.nl/standard/ecss-q-st-70-80c-processing-and-quality-assurance-requirements-for-metallic-powder-bed-fusion-technologies-for-space-applications-30-july-2021/ | Sourced |
| Numbers, titles and status of ISO/ASTM 52900:2021, 52904:2024, 52909:2024, 52941 (2026 edition), 52942:2020 and 52920:2023 | ISO catalogue pages Reference 26 https://www.iso.org/standard/74514.html Reference 27 https://www.iso.org/standard/82919.html Reference 28 https://www.iso.org/standard/87956.html Reference 29 https://www.iso.org/standard/86784.html Reference 30 https://www.iso.org/standard/74949.html Reference 31 https://www.iso.org/standard/76911.html | Sourced |
| The relative values in Fig. 4 (first liner = 100, roughness about 50, pressure drop at most 80) | Our plot (from NASA statements; the pressure drop is an upper bound) | Our calculation |
| Results of printing and evaluating a metal part in orbit, flight heritage of metal printed satellite parts, flight heritage and independent verification of HR-1 and GRX-810, standardization of PDTA, application of fracture control to printed-specific defects, and ASTM-only standards | Could not be confirmed in primary sources within this survey, so not stated (this article) | Commentary |
| The readings "surface roughness is a design input", "printable and suited to printing differ", "publishing failures grows standards" and "a process qualified on the ground cannot be taken to orbit", the view that a standard is not a guarantee, and analogies and their limits | Our organization and commentary based on the published material | Commentary |
| Figs. 1 and 9 are AI-generated concept images, and Figs. 2 to 8 are explanatory drawings | Note by this article | Commentary |
Last updated: 17 October 2026. Sources are limited to primary materials (NASA reports, presentations, standards and a mission page, ECSS, ISO catalogue pages, an official L3Harris page). Company announcements are treated as company statements. Fig. 4 shows relative values we plotted from NASA statements. Results of printing and evaluating metal in orbit, flight heritage of metal printed satellite parts, independent verification of HR-1 and GRX-810, and standardization of PDTA could not be confirmed and are not stated. The detailed cause of the failure case is kept to the published abstract and is not speculated on. Figs. 1 and 9 are AI-generated concept images and do not depict real facilities or products.